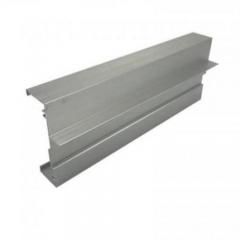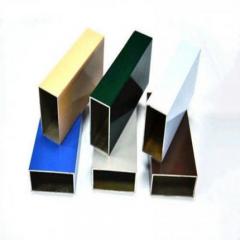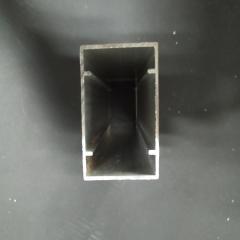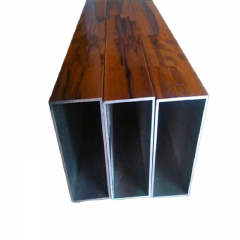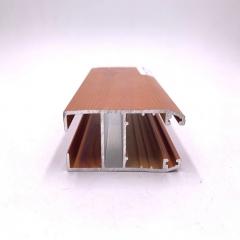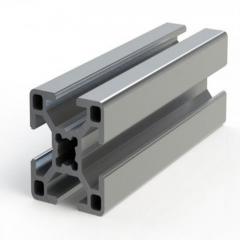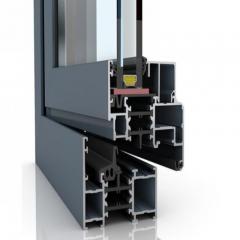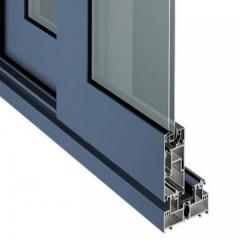
When you're standing in a doorway, you probably don't think about what's holding everything together. Yet those vertical aluminum components lining the opening—known as aluminum door jamb extrusions—are doing critical work behind the scenes. These specialized profiles serve as the backbone of modern aluminum door frames, providing the structural foundation that keeps your doors functioning smoothly for decades.
So what exactly are these components? Aluminum door jamb extrusions are precision-manufactured vertical frame members that line the sides and top of door openings. Unlike generic aluminum door and frame assemblies, door jamb extrusions are specifically engineered to handle the unique stresses of door operation—repeated opening cycles, hardware loads, and environmental exposure.
Think of the door jamb as the interface between your wall and your door. This extruded frame component performs three essential functions that make modern doorways possible:
What sets aluminum frame extrusion apart from wood or steel alternatives is its remarkable consistency. Every inch of an extruded profile maintains identical dimensions, ensuring hardware aligns perfectly and weatherstripping seats uniformly along the entire length.
Imagine pushing heated aluminum—softened to roughly 900°F—through a precision-cut steel die. That's the essence of aluminum extrusion, and it's what makes these components possible. The process begins with cylindrical aluminum billets loaded into a hydraulic press. Under immense pressure, the softened metal flows through the die opening, emerging as a continuous profile with the exact cross-sectional shape needed for your application.
This manufacturing method offers advantages you simply can't achieve with other fabrication techniques. Complex internal chambers for thermal breaks, integrated screw chases for hardware attachment, and precise weatherstrip grooves all emerge in a single operation. The same extrusion technology that creates aluminum rails for sliding doors also produces the intricate profiles required for commercial entrance systems.
The result? Aluminum door frames with tolerances measured in thousandths of an inch. Whether you're installing a single residential entry or hundreds of commercial storefronts, each jamb section matches the next perfectly—eliminating the fitting headaches common with site-fabricated alternatives.
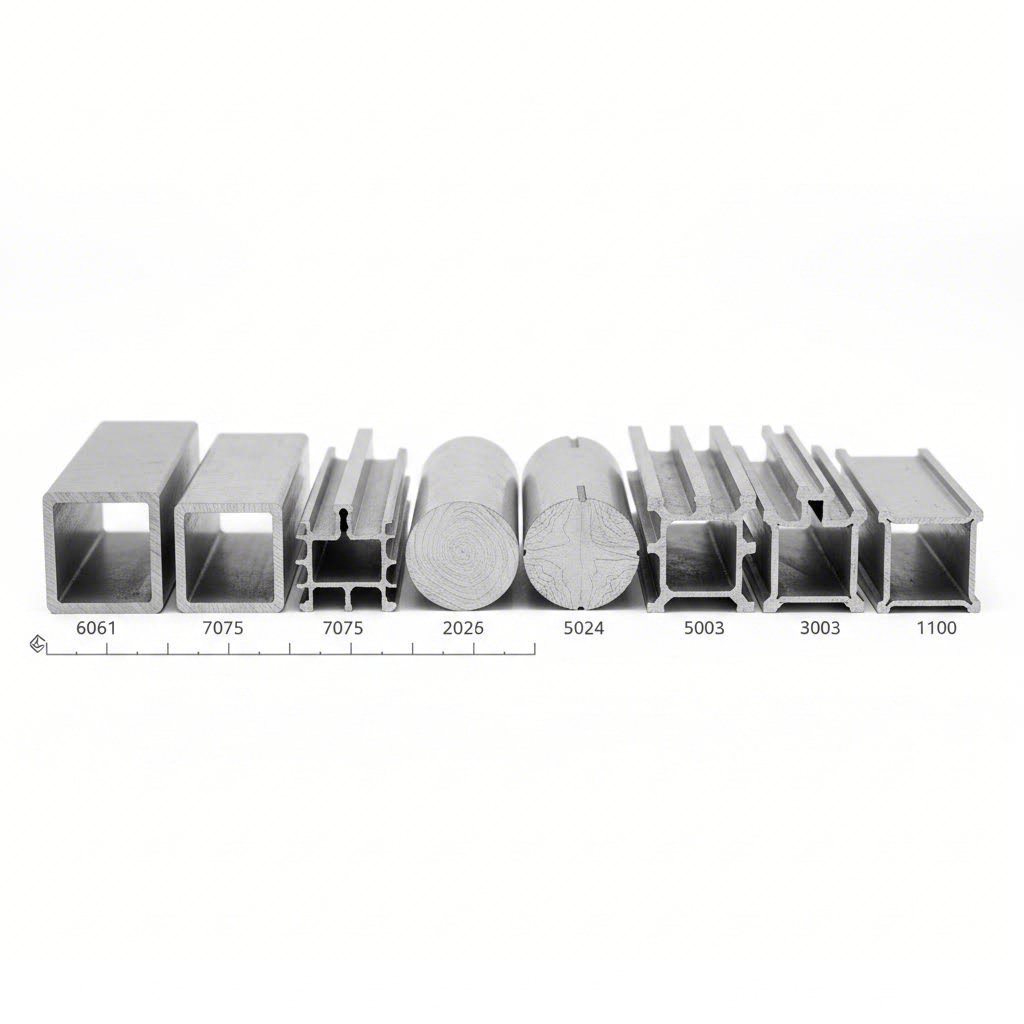
Here's something many buyers overlook: not all aluminum is created equal. The alloy running through your aluminum door frame determines everything from how well it resists coastal salt spray to whether it can support a 300-pound commercial entry door. Understanding these material differences helps you specify the right product—and avoid costly replacements down the road.
Aluminum alloys are identified by four-digit numbers, each representing a specific blend of aluminum with elements like magnesium, silicon, copper, or zinc. These additions dramatically alter the metal's behavior. Some combinations excel at corrosion resistance. Others prioritize raw strength. For aluminum door jamb extrusions, the sweet spot lies in alloys that balance multiple performance factors while remaining easy to manufacture.
Walk into any commercial building with aluminum entrances, and you're likely looking at 6063 alloy. This magnesium-silicon blend has dominated architectural extrusion for decades—and for good reason. Its composition (roughly 0.4% silicon and 0.7% magnesium) creates an alloy that flows beautifully through extrusion dies, producing the sharp corners and intricate details modern aluminum door frame profiles demand.
What makes 6063 particularly attractive for extruded aluminum panels and door jambs? Three key characteristics:
You'll encounter 6063 in two common temper conditions: T5 and T6. The difference matters more than you might think. T5 temper means the extrusion was cooled from the elevated extrusion temperature and then artificially aged. T6 temper adds a solution heat treatment step before aging, resulting in higher strength but also higher cost. For most aluminum extrusions for panels and standard door applications, T5 provides adequate strength at better economy.
Sometimes 6063 isn't enough. Heavy commercial doors, high-security applications, or aluminum panel extrusions subject to significant structural loads may require stronger alternatives. This is where alloy selection becomes a balancing act.
Consider 6061 alloy—often called the "workhorse" of structural aluminum. With higher silicon and magnesium content plus copper additions, 6061-T6 delivers roughly 40% greater yield strength than 6063-T6. Sounds ideal, right? The trade-off appears during manufacturing: 6061 is harder to extrude, produces rougher surfaces, and responds less uniformly to anodizing. You gain strength but sacrifice the pristine appearance expected in architectural work.
Then there's 6005, which occupies the middle ground. It offers strength approaching 6061 while maintaining better extrudability than that alloy—though still not matching 6063's surface finish. For structural applications where appearance is secondary, 6005-T5 often represents the optimal compromise.
| Alloy | Typical Applications | Corrosion Resistance | Best Use Cases |
|---|---|---|---|
| 6063-T5/T6 | Architectural door frames, window systems, decorative trim | Excellent | Visible applications requiring superior finish quality and anodizing response |
| 6061-T6 | Structural components, heavy-duty frames, industrial equipment | Good | High-load applications where strength outweighs aesthetic requirements |
| 6005-T5 | Transportation, structural profiles, ladder rails | Good to Excellent | Applications needing higher strength than 6063 with reasonable surface quality |
When specifying aluminum door jamb extrusions, match the alloy to your actual requirements. A residential entry door doesn't need 6061's structural capacity—and paying for it while accepting inferior aesthetics makes little sense. Conversely, specifying 6063 for an industrial facility with oversized blast-resistant doors invites premature failure. Understanding these trade-offs puts you in control of both performance and budget.
With alloy selection clarified, the next critical decision involves surface treatment—where finish options range from raw mill surfaces to high-performance coatings engineered for decades of exposure.
You've selected the right alloy for your aluminum door jamb extrusions—now what? The finish you choose determines whether your installation looks pristine after fifteen years or develops unsightly corrosion within months. Think of surface finishing as your extrusion's armor, protecting the underlying metal while delivering the aesthetic impact your project demands.
Three primary finish categories dominate the aluminum door extrusion market, each offering distinct advantages depending on your installation environment and performance requirements.
Mill finish represents raw aluminum straight from the extrusion press. While economical, this uncoated surface relies solely on aluminum's natural oxide layer for protection. You'll find mill finish acceptable for concealed applications or temporary installations, but visible architectural elements typically warrant enhanced treatment.
Ever wonder why commercial aluminium glass door frame systems maintain their appearance through decades of heavy use? Anodizing is often the answer. This electrochemical process doesn't simply coat the aluminum—it transforms the surface itself into an integral oxide layer that becomes part of the metal.
Here's how it works: your extrusion is submerged in an acid electrolyte bath while electrical current passes through the solution. This controlled oxidation creates a porous aluminum oxide layer measuring 0.5 to 1.0 mils thick for architectural applications. The resulting surface is significantly harder than raw aluminum, resisting scratches from keys, rings, and daily contact that would quickly mar untreated metal.
What makes anodizing particularly valuable for aluminium window frame extrusions and door jambs?
For coastal installations, specify Class I anodizing with a minimum 0.7-mil thickness. This heavier coating provides superior salt spray resistance compared to standard Class II finishes—a critical distinction when your aluminum extrusion panels face ocean exposure.
Need precise color matching or enhanced UV resistance? Powder coating opens possibilities anodizing simply cannot match. This thermoset polymer finish is applied electrostatically as a dry powder, then cured at elevated temperatures to form a durable, uniform coating.
Imagine specifying your door frames in any RAL or custom color—powder coating makes this practical. The technology accommodates everything from subtle earth tones to bold corporate colors, with texture options ranging from smooth gloss to wrinkled matte finishes. For architectural aluminum door extrusion applications requiring specific aesthetic integration, powder coating delivers unmatched flexibility.
Beyond aesthetics, powder coating provides:
For extreme environments—think Florida beach resorts or Arizona desert installations—PVDF (polyvinylidene fluoride) coatings represent the premium tier. These fluoropolymer finishes, commonly known by the brand name Kynar, deliver exceptional color retention and weathering resistance across 20+ year lifespans. The higher cost is justified for high-visibility architectural projects where finish failure would require costly replacement.
| Finish Type | Durability Rating | Color Options | Cost Level | Recommended Environments |
|---|---|---|---|---|
| Mill Finish | Low to Moderate | Natural aluminum only | Lowest | Concealed applications, interior industrial |
| Anodized (Class II) | High | Limited architectural colors | Moderate | Interior commercial, moderate exterior exposure |
| Anodized (Class I) | Very High | Limited architectural colors | Moderate-High | Coastal, high-humidity, high-traffic areas |
| Powder Coated (Polyester) | High | Unlimited RAL and custom colors | Moderate | General exterior, interior commercial |
| PVDF/Kynar Coating | Exceptional | Unlimited RAL and custom colors | Highest | Severe coastal, extreme UV, high-profile architectural |
Selecting the right finish comes down to matching protection level with environment. Interior commercial applications—retail stores, office lobbies, healthcare facilities—typically perform well with standard anodizing or polyester powder coating. These environments expose frames to handling and cleaning rather than weather extremes.
Exterior installations demand more careful evaluation. A storefront in Minneapolis faces different challenges than one in Miami. Northern climates bring freeze-thaw cycling and road salt exposure; southern coastal areas deliver relentless UV radiation and salt-laden air. For high-humidity environments like natatoriums or commercial kitchens, anodizing's integral oxide layer often outperforms surface coatings that moisture might eventually undermine.
When budget permits, combining treatments offers optimal protection. A clear anodized base layer by powder coating provides both the corrosion barrier of electrochemical treatment and the color flexibility of polymer finishes—a specification increasingly common in demanding architectural applications.
Where will your aluminum door jamb extrusions actually live? The answer shapes every specification decision—from alloy selection to finish type to profile geometry. A residential front entry experiences fundamentally different stresses than a busy hospital corridor or a cargo trailer bouncing down highways. Understanding these application-specific demands helps you match the right extrusion to your exact use case.
Let's walk through the major application categories, examining what makes each unique and how those differences translate into specification requirements.
Picture a retail entrance during holiday shopping season. Hundreds of customers streaming through daily, carts bumping against frames, automatic operators cycling continuously. Commercial storefronts demand aluminum door frame profiles engineered for punishment that would destroy residential-grade alternatives within months.
Key considerations for commercial storefront applications:
For aluminum sliding door frame applications in commercial settings—think patio restaurants or conference room dividers—the aluminum sliding glass track must handle repeated operation while maintaining smooth, quiet performance. These installations often integrate with automated systems, adding electrical routing requirements to the jamb profile design.
Residential projects present different priorities. Here, aesthetic appeal often rivals durability in importance. Homeowners want entry systems that complement architectural styles while providing security and energy efficiency.
Residential aluminum door jamb considerations differ from commercial in several ways:
For interior residential applications like aluminum cabinet door extrusion projects or closet systems, lighter-gauge profiles suffice since these installations avoid weather exposure and experience minimal operational stress.
Hotels, hospitals, and senior living facilities combine commercial traffic levels with elevated hygiene and safety requirements. These environments demand extrusions that facilitate frequent cleaning while withstanding gurney impacts, luggage carts, and continuous use.
Specify for hospitality and healthcare with these factors in mind:
Industrial facilities introduce challenges rarely encountered in commercial or residential settings. Chemical exposure, extreme temperatures, heavy equipment traffic, and specialized security needs all influence extrusion selection.
Consider these industrial-specific requirements:
Aluminum trailer door frame extrusions represent a particularly demanding specialty niche. These components must withstand constant vibration, road shock, temperature cycling, and repeated latching operations while maintaining weathertight seals. Successful trailer applications typically specify:
Shower enclosures and bathroom applications present yet another specialty environment. These installations require profiles resistant to constant moisture, soap residue, and cleaning chemicals. Anodized finishes typically outperform powder coatings in wet environments, as the integral oxide layer won't delaminate from prolonged water exposure. Aluminium sliding door rails in shower applications must resist corrosion while providing smooth, reliable operation despite mineral deposits from hard water.
Whatever your application, matching extrusion specifications to actual operating conditions prevents premature failure and ensures long-term satisfaction. The next consideration—thermal break technology—becomes increasingly critical as energy codes tighten across all building types.
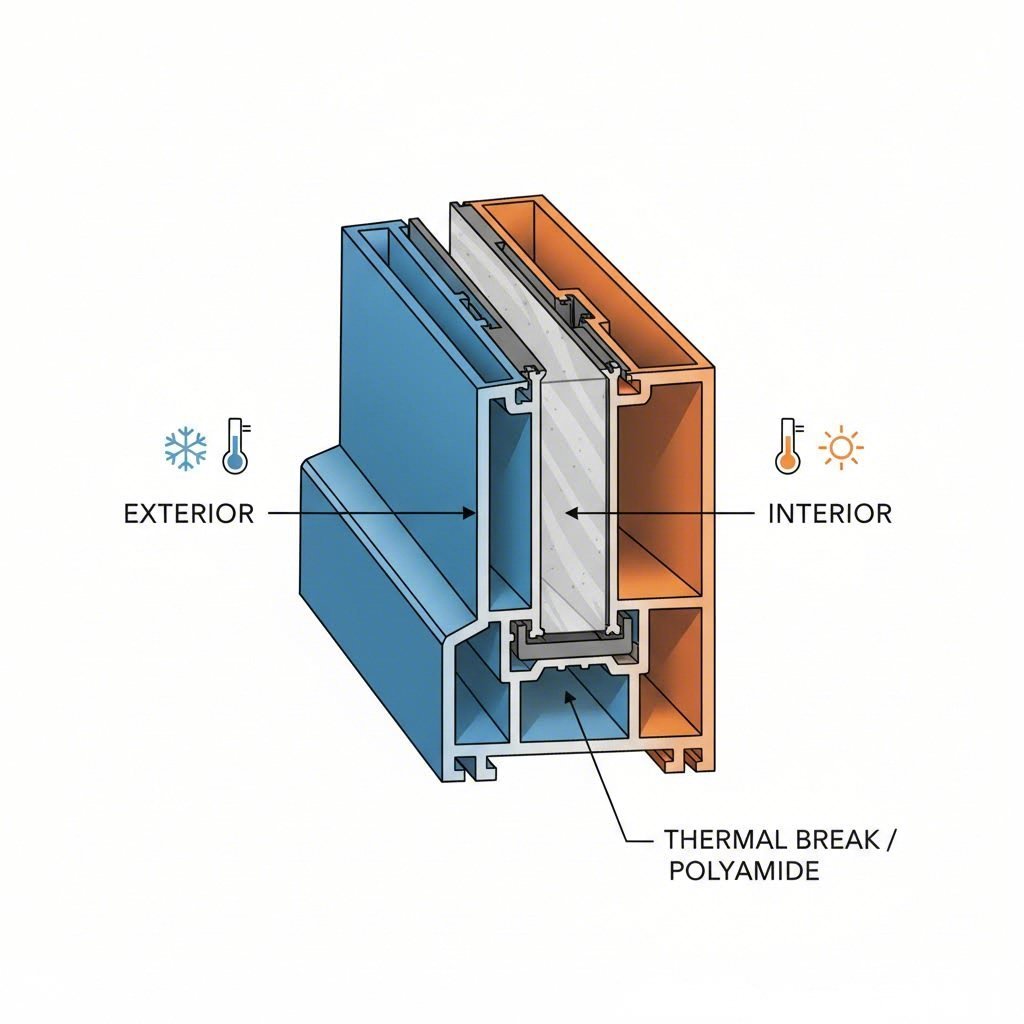
Ever touched an aluminum window frame on a freezing winter morning? That cold surface tells you something important: metal conducts heat remarkably well. Without intervention, your extruded aluminum door frame becomes a thermal highway—transferring conditioned indoor air straight to the outdoors and driving up energy bills. Thermal break technology solves this problem, and understanding how it works helps you specify door systems that perform efficiently year-round.
So what exactly is a thermal break? Picture your aluminum door frame profile split into two separate sections—one facing indoors, one facing outdoors—connected by an insulating barrier that blocks heat flow between them. This barrier, typically made from reinforced polyamide (a high-strength engineered plastic), creates a thermal separation within the extrusion itself. Heat energy attempting to travel through the frame hits this insulating zone and largely stops.
Thermal breaks transform aluminum door frame extrusions from energy liabilities into high-performance building components. Without this technology, aluminum's thermal conductivity—roughly 1,500 times greater than polyamide—creates a direct path for heat transfer. In winter, warm interior air meets cold aluminum, cooling rapidly and creating uncomfortable drafts near doorways. In summer, the process reverses, with hot exterior surfaces radiating heat inward.
Two manufacturing methods dominate thermal break production:
The performance difference is substantial. Standard aluminum frames typically exhibit U-factors around 1.0 to 1.2 BTU/hr·ft²·°F. Add quality thermal breaks, and that figure drops to 0.4 to 0.6—representing a 50% or greater improvement in thermal resistance. For your heating and cooling systems, this translates directly into reduced runtime and lower utility costs.
Beyond energy savings, thermal breaks address condensation resistance—a critical concern in humid climates or buildings with indoor pools and commercial kitchens. When warm, moist interior air contacts cold frame surfaces, water droplets form. This condensation damages finishes, promotes mold growth, and accelerates hardware corrosion. Thermal break profiles maintain interior surface temperatures above the dew point, keeping frames dry even when exterior temperatures plummet.
Energy codes have tightened dramatically over the past decade. What was once optional has become mandatory in most jurisdictions. Understanding when thermal breaks are required—and how to demonstrate compliance—prevents costly specification errors and project delays.
Commercial buildings in climate zones 4 through 8 now require thermal break technology for virtually all metal-framed exterior door assemblies to meet ASHRAE 90.1 and IECC energy code requirements.
Compliance verification centers on two key metrics:
Does every project need thermal breaks? Not necessarily. Interior aluminum door jamb extrusions separating conditioned spaces don't require thermal separation—there's no temperature differential driving heat transfer. Similarly, unconditioned spaces like parking garages or warehouse loading docks may be exempt from thermal performance requirements. However, any exterior door in a climate-controlled building almost certainly needs thermal break technology to meet current codes.
The cost and complexity difference between standard and thermal break profiles is real but often overstated. Expect thermal break extrusions to cost 25-40% more than comparable non-thermal profiles. Manufacturing complexity increases as well—these profiles require additional processing steps and tighter quality control. For projects where codes mandate thermal breaks, this premium is unavoidable. For projects in mild climates or with exempt applications, standard profiles offer cost savings without compliance concerns.
When specifying thermal break door systems, request NFRC (National Fenestration Rating Council) certified performance data. These third-party verified ratings ensure the products actually deliver claimed thermal performance—protecting you from underperforming substitutions that could trigger code violations during inspection.
You've decided on thermal break requirements and finish specifications—but have you considered whether aluminum is actually the right material for your project? While aluminum door jamb extrusions dominate commercial construction, they're not automatically the best choice for every application. Steel, wood, and vinyl each bring legitimate advantages depending on your priorities. Let's compare honestly so you can make an informed decision.
Imagine hauling door frames up three flights of stairs on a renovation project. Suddenly, material weight becomes very personal. Aluminum weighs roughly one-third as much as steel—a difference installers notice immediately. That 8-foot alum door frame you can carry solo? Its steel equivalent might require two workers and careful maneuvering.
But lighter doesn't always mean better. Consider these trade-offs:
Dimensional stability separates these materials over time. Wood absorbs moisture, swelling in humid summers and shrinking during dry winters. This movement affects door operation and seal integrity—you've likely experienced sticky doors that suddenly swing freely when seasons change. Aluminum maintains consistent dimensions regardless of humidity, ensuring hardware alignment and weatherstrip contact remain constant. Steel shares this stability but introduces rust concerns without proper finishing.
That vinyl door jamb costs half as much as aluminum sliding alternatives—sounds like a bargain, right? Not so fast. Initial purchase price tells only part of the story. Factor in maintenance, longevity, and replacement cycles, and the economics shift considerably.
Here's where aluminum door jamb extrusions demonstrate compelling value:
Steel delivers unmatched security but demands ongoing maintenance. Exterior steel frames require periodic inspection and touch-up to prevent rust progression. Miss a scratch on a coastal installation, and corrosion spreads beneath surrounding paint. Wood offers warmth and traditional appeal but needs refinishing every few years and eventual replacement as moisture damage accumulates.
| Material | Weight (Relative) | Corrosion Resistance | Maintenance Requirements | Cost Range | Best Applications |
|---|---|---|---|---|---|
| Aluminum | Low (1x) | Excellent | Minimal—periodic cleaning only | Medium-High | Commercial storefronts, high-traffic entries, coastal installations, extruded aluminum slide systems |
| Steel | High (3x) | Poor without coating | Regular inspection, touch-up painting | Medium-High | Maximum security, detention, blast-resistant, fire-rated assemblies |
| Wood | Medium (1.5x) | Poor—susceptible to rot | Periodic refinishing, seal maintenance | Medium-High | Traditional residential, historic preservation, interior applications |
| Vinyl | Lowest (0.7x) | Excellent | Minimal—cleaning only | Low | Budget residential, low-traffic entries, replacement windows |
When does each material make the most sense? Choose aluminum for commercial durability, dimensional consistency, and long-term value. Specify steel when security requirements demand maximum resistance to forced entry. Select wood for residential projects prioritizing traditional aesthetics and natural insulating properties. Consider vinyl for budget-conscious residential installations with modest performance expectations.
The sustainability angle increasingly influences material selection. Aluminum's recyclability—with recycled content requiring just 5% of the energy needed for primary production—appeals to green building certifications. Wood offers renewable sourcing but faces durability limitations. Steel recycling is well-established but energy-intensive. Vinyl recycling infrastructure remains limited, with most end-of-life material heading to landfills.
Understanding these material trade-offs positions you to make confident specification decisions. But once you've chosen aluminum, another question emerges: should you use standard catalog profiles or invest in custom extrusions tailored to your exact requirements?
You've decided aluminum is right for your project—but now comes a question that trips up many specifiers: should you order from a catalog of standard profiles or invest in custom extrusions designed specifically for your application? The answer depends on factors that most suppliers mention but rarely explain in practical terms. Let's break down the economics, timelines, and decision criteria so you can choose confidently.
Standard aluminum door jamb extrusions are mass-produced using existing dies, offering immediate availability and predictable pricing. Custom profiles, by contrast, require developing new tooling specific to your cross-sectional design. Neither option is universally superior—the right choice depends entirely on your project's unique requirements.
Custom aluminum track extrusion development isn't cheap, but it's not as prohibitive as many assume. The question isn't whether you can afford custom tooling—it's whether your project justifies the investment. Several scenarios tip the balance toward bespoke profiles:
Conversely, standard extruded aluminum track profiles make sense when your requirements align with common industry specifications. Modular workstations, basic structural framing, display systems, and general-purpose applications rarely need custom solutions. Why pay for die development when existing profiles already meet your functional needs?
Here's where projects often stall: nobody explains what die creation actually involves. When you commission a custom aluminum extrusion track, your manufacturer must machine a precision steel die matching your exact cross-sectional profile. This die—essentially a thick steel plate with your shape cut through it—mounts in the extrusion press and forms every foot of material you order.
Typical die tooling investments range from $500 for simple shapes to $5,000 or more for complex multi-cavity dies with intricate internal features. Factors affecting tooling cost include:
The good news? Dies typically last for years of production, often producing hundreds of thousands of pounds of extrusion before requiring replacement. Once you've made the initial investment, reorders use existing tooling at no additional die cost.
Minimum order quantities present another practical consideration. Custom profiles often carry MOQs ranging from 500 to 2,000 pounds—ensuring the production run justifies setup time and press allocation. Standard profiles from distributor stock might ship in quantities as small as single lengths. For small projects or prototyping, this flexibility can outweigh the benefits of custom geometry.
Lead times differ substantially between approaches. Standard profiles sitting in warehouse inventory ship within days. Custom extrusions require die development (typically 2-4 weeks), by scheduled production time (another 2-4 weeks), plus any finishing operations. Plan for 6-8 weeks minimum from order to delivery for custom profiles—and build buffer for unexpected delays.
How does order volume affect unit pricing? Simple economics apply: larger orders spread fixed costs across more material, reducing per-foot pricing. A 500-pound minimum order absorbs the same setup costs as a 5,000-pound run, making the smaller quantity significantly more expensive per unit. When evaluating custom versus standard, calculate your total project requirements and any anticipated reorders—the full picture often reveals better value than initial quotes suggest.
Smart specification starts with honest assessment: do your requirements genuinely demand custom profiles, or are you solving a standard problem with unnecessary complexity? For projects requiring precise integration with existing hardware or proprietary system development, custom aluminum extrusion track profiles deliver value that justifies their investment. For general construction applications using common configurations, standard catalog profiles offer faster delivery and lower entry costs without compromising performance.
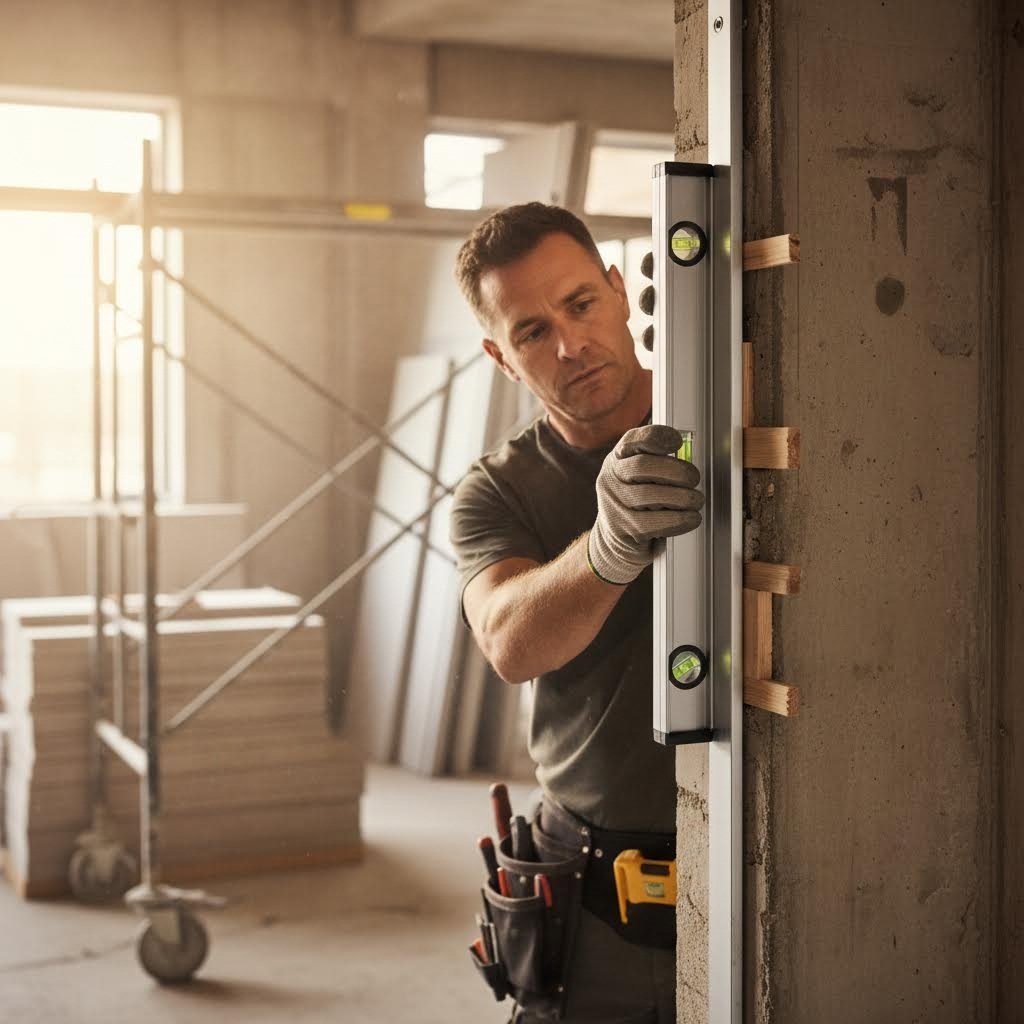
You've selected the perfect aluminum door jamb extrusions, specified the right alloy and finish, and your custom or standard profiles have arrived on site. Now comes the moment that determines whether your investment performs flawlessly for decades—or creates headaches within months. Proper installation transforms quality components into a functional door system, while shortcuts invite alignment problems, air leakage, and premature hardware failure.
What separates professional aluminum frame installation from amateur attempts? Attention to preparation, precision alignment, and proper fastening techniques. Let's walk through the complete process so you can execute—or supervise—installations that meet commercial standards.
Before your aluminum sliding door track or entry jamb touches the opening, preparation work determines success. Rushing this phase guarantees problems later.
Start with these critical verification steps:
For exterior installations, moisture management begins now. Install appropriate flashing at the sill and head locations before the frame goes in. Improper flashing allows water infiltration behind the frame—invisible damage that progresses until costly repairs become unavoidable. Integrate your aluminum sliding door tracks or jamb assemblies with the building's weather-resistive barrier for continuous protection.
With preparation complete, frame installation proceeds through a systematic sequence. Following these steps in order prevents the backtracking and adjustment that plague disorganized installations:
Fastener selection matters as much as technique. For wood substrates, use minimum #10 screws with sufficient length to penetrate framing by at least 1-1/2 inches. For masonry or concrete, one-piece anchor bolts sized per manufacturer specifications provide secure attachment. Avoid using anchors with separate expansion sleeves in hollow masonry—these pull out under operational loads.
Even experienced installers occasionally make errors that compromise aluminium sliding door track and jamb performance. Watch for these frequent problems:
Threshold integration completes the installation. Set thresholds in continuous caulk beads to prevent water penetration at this vulnerable junction. Shim as necessary to achieve level positioning, and verify that door bottom seals contact the threshold uniformly across the full width.
For exterior applications, seal the frame perimeter with appropriate caulking. Apply continuous beads along all four sides where the frame meets the wall surface—this final step prevents air infiltration and water entry that would undermine your entire installation effort.
With proper installation complete, your aluminum door jamb extrusions are positioned to deliver years of reliable service. But even the best installation requires ongoing attention to maintain peak performance over time.
Your aluminum door jamb extrusions are installed, aligned perfectly, and operating smoothly. Now what? The difference between frames that look pristine after fifteen years and those showing premature wear often comes down to maintenance—or the lack of it. Fortunately, aluminum requires far less attention than wood or steel alternatives, but "low maintenance" doesn't mean "no maintenance."
Environmental exposure dramatically influences how often your frames need attention. A protected interior doorway and a coastal storefront face entirely different challenges. Understanding these differences helps you establish cleaning schedules that protect your investment without wasting effort on unnecessary tasks.
Remember how salt air corrodes steel almost immediately? Aluminum behaves differently—but it's not immune. Coastal environments deposit salt films that trap moisture against surfaces, accelerating oxidation on bare aluminum edges and potentially undermining powder-coated finishes over time. According to industry maintenance guidelines, installations within 5 miles of coastlines require monthly cleaning to prevent cumulative damage.
Your cleaning approach should match your finish type:
Anodized Finishes: The integral oxide layer resists most environmental exposure, but still benefits from regular cleaning. Use mild soapy water and a soft cloth or sponge, rinsing thoroughly and drying completely. For stubborn deposits, a light application of lacquer thinner on a soft cloth works well—just keep it away from rubber gaskets and weatherstripping. After cleaning, applying automotive wax enhances appearance and adds protective barrier against future soiling.
Powder-Coated Finishes: These polymer surfaces demand gentler treatment. Never use acetone, lacquer thinner, or aggressive solvents that could damage the coating. Stick with mild soap and water, using a soft bristle brush for textured finishes. Rinse one section at a time to prevent cleaning solutions from drying on surfaces. Automotive wax works equally well on powder-coated aluminum tracks and jamb surfaces.
Mill Finish (Bare Aluminum): Uncoated aluminum naturally develops an oxide layer that appears as dark, metallic-looking residue when wiped. This oxidation is normal and doesn't compromise structural integrity. Use a fine Scotch-Brite pad to gently remove heavy oxidation, then wipe clean and apply car wax for ongoing protection. Pay special attention to exposed edges and weep holes where oxidation concentrates.
Regardless of finish type, certain practices apply universally:
Consistent scheduling prevents small issues from becoming expensive problems. Manufacturer maintenance guides recommend organizing tasks by frequency based on your installation environment:
Monthly Tasks (Coastal Locations) / Quarterly Tasks (Standard Locations):
Semi-Annual Tasks:
Annual Tasks:
Every Five Years:
Even well-maintained aluminum door jamb extrusions eventually show signs indicating replacement rather than continued repair. Watch for these conditions:
Working with experienced manufacturers provides advantages beyond initial product quality. Established suppliers maintain component specifications, enabling replacement parts that match original installations even years later. Technical support resources help diagnose problems and identify whether repair or replacement makes economic sense for your specific situation.
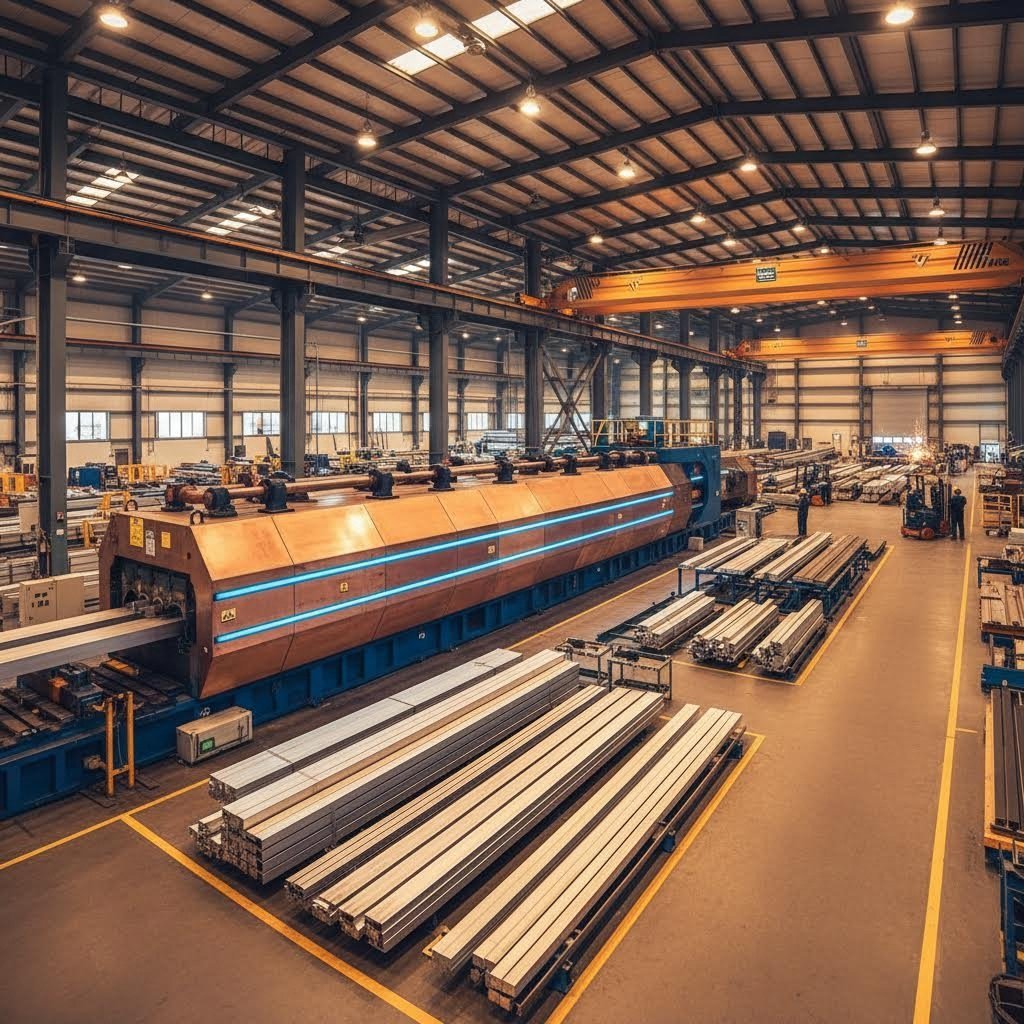
You've navigated alloy selection, finish specifications, thermal break requirements, and installation best practices. Now comes the decision that ties everything together: choosing a manufacturing partner capable of delivering aluminum door jamb extrusions that meet your exact requirements. The wrong supplier creates headaches ranging from missed deadlines to out-of-spec profiles that complicate installation. The right partner becomes an extension of your project team—solving problems before they emerge and supporting your success from initial quote through final delivery.
How do you evaluate potential extrusion suppliers? Start with a systematic specification checklist, then assess manufacturing capabilities that indicate whether a partner can actually deliver what your project demands.
Before contacting any manufacturer, document your requirements clearly. Vague specifications invite misunderstandings and costly revisions. Walk through these critical selection criteria to ensure complete alignment between your needs and supplier capabilities:
Document these specifications in writing before requesting quotes. Clear requirements enable accurate pricing and prevent scope creep that derails budgets and schedules.
With specifications documented, you're ready to evaluate potential manufacturing partners. Not all extrusion suppliers offer equal capabilities—and claims on websites don't always match reality. Here's what distinguishes capable partners from those who'll leave you scrambling:
Extrusion Press Capacity Range: The size of a manufacturer's extrusion presses determines what profiles they can produce. Small presses (under 1,000 tons) handle simple shapes and smaller cross-sections. Complex architectural profiles with multiple chambers or large dimensions require heavy-tonnage equipment. Look for manufacturers operating diverse press fleets—companies with equipment ranging from 600T to 5500T can handle virtually any aluminum tracking requirement, from delicate aluminum extrusion slider channels to massive structural profiles.
Surface Treatment Capabilities: Does your potential partner perform finishing in-house or outsource to third parties? Integrated facilities maintain tighter quality control and faster turnaround. Comprehensive treatment capabilities should include anodizing (in architectural colors like champagne, bronze, and black), powder coating with extensive color matching, and specialized finishes like PVDF for extreme environments or micro-arc oxidation for enhanced durability.
CNC Machining for Custom Cuts: Raw extrusion is just the starting point. Most projects require precision cutting, drilling, miter joints, or complex machining to create installation-ready components. Partners with advanced CNC machining centers deliver extruded aluminium track sections cut to exact lengths with drilled mounting holes positioned precisely where your hardware requires—eliminating field fabrication and associated quality variability.
Technical Support From Die Development Through Production: The best manufacturing relationships extend beyond order processing. Look for partners whose engineering teams assist with die design optimization, material selection guidance, and finish recommendations based on your application requirements. This technical collaboration prevents specification errors that create problems during installation.
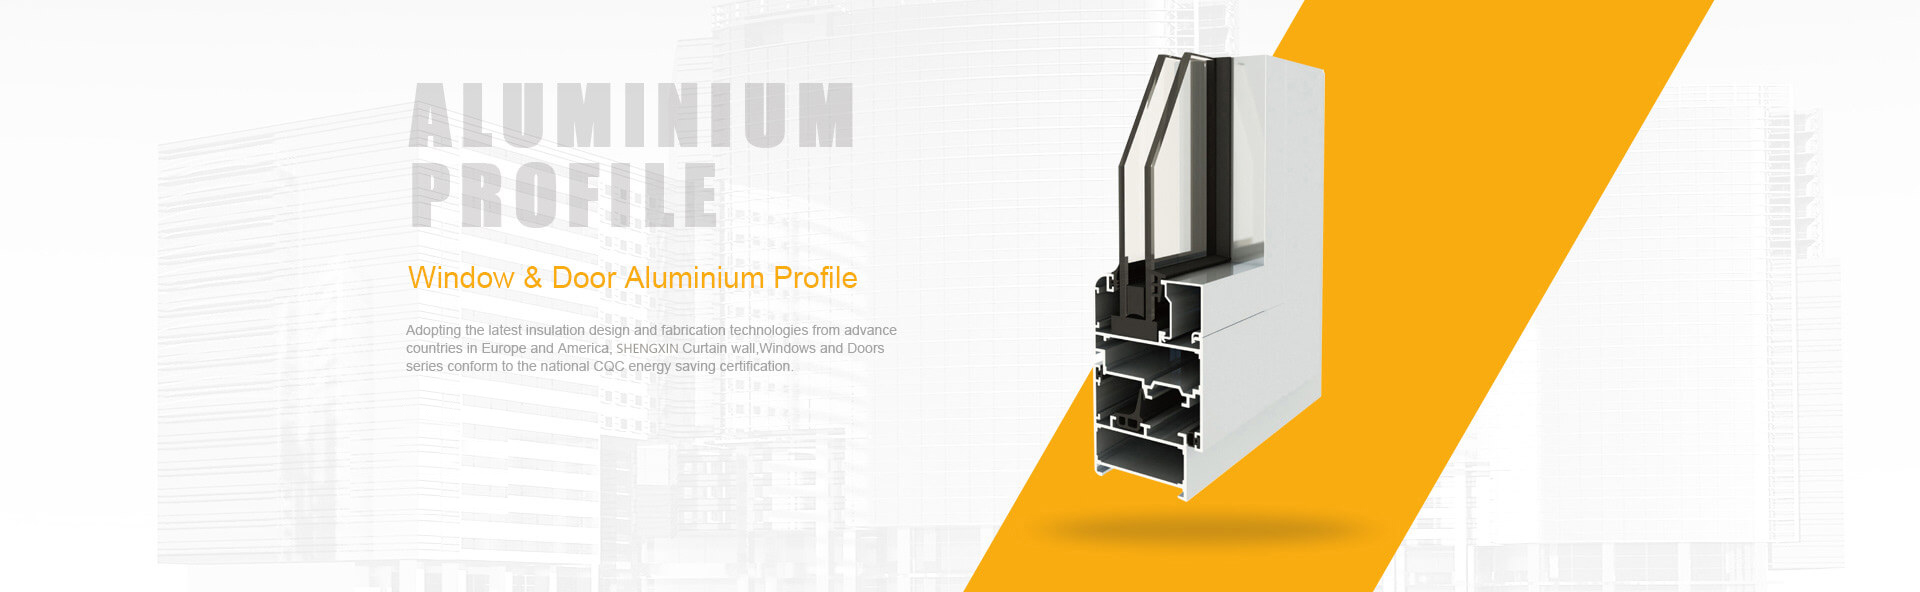
For projects requiring comprehensive aluminum extrusion and deep processing services, Shengxin Aluminium exemplifies the full-service manufacturing capability serious projects demand. With over 30 years of industry experience and 35 advanced extrusion presses ranging from 600T to 5500T, their facility handles everything from standard aluminum slide track channel profiles to complex custom architectural extrusions. Their integrated surface treatment capabilities—including anodizing in custom colors, powder coating, PVDF, and micro-arc oxidation—eliminate the coordination headaches of multi-vendor supply chains. State-of-the-art CNC machining centers provide precise cutting, drilling, and bending to exact specifications, delivering installation-ready components rather than raw material requiring field fabrication.
What makes this end-to-end approach valuable? Consider the alternative: sourcing raw extrusions from one supplier, finishing from another, and machining from a third. Each handoff introduces quality variability, communication gaps, and scheduling complexity. Integrated manufacturers maintain accountability throughout the process—and offer factory-direct pricing that eliminates distributor markups eating into your budget.
Before committing to any supplier, request these verification items:
The effort invested in thorough supplier evaluation pays dividends throughout your project. Partners with genuine manufacturing depth solve problems proactively, deliver consistent quality, and support your installation teams with technical resources that prevent field complications. Those lacking capabilities shift problems downstream—where you absorb the cost and schedule impact.
Your aluminum door jamb extrusions represent a long-term investment in building performance. Selecting a manufacturing partner with comprehensive capabilities, proven expertise, and genuine technical support positions your project for success from specification through decades of reliable service.
Aluminum door jamb extrusions are precision-manufactured vertical frame members that line door openings, providing three essential functions: structural integrity to transfer door weight and operational forces into the wall structure, weather sealing through integrated channels that accept weatherstripping, and hardware mounting with reinforced areas for hinges, strike plates, and locking mechanisms. They're used in residential entries, commercial storefronts, hospitality environments, industrial facilities, and specialty applications like shower enclosures and trailer doors.
The 6063-T5 and 6063-T6 alloys are industry standards for aluminum door jamb extrusions due to their excellent extrudability, superior surface quality, and outstanding response to anodizing and powder coating. For applications requiring higher strength, 6061-T6 offers approximately 40% greater yield strength but with rougher surface finishes. The 6005-T5 alloy provides a middle-ground option with strength approaching 6061 while maintaining better extrudability for structural applications where appearance is secondary.
Choose anodizing when you need integral protection that cannot peel or chip, uniform coverage including interior channels, and excellent durability in high-humidity or wet environments. Select powder coating when precise color matching is required, unlimited RAL colors are needed, or enhanced UV resistance is important. For extreme environments like coastal areas or intense sun exposure, PVDF coatings offer exceptional color retention over 20+ year lifespans. Consider combining both treatments for optimal protection in demanding architectural applications.
Thermal break technology is required for virtually all metal-framed exterior door assemblies in commercial buildings located in climate zones 4 through 8 to meet ASHRAE 90.1 and IECC energy code requirements. Thermal breaks reduce U-factors from 1.0-1.2 to 0.4-0.6, representing over 50% improvement in thermal resistance. Interior door jambs separating conditioned spaces and doors in unconditioned areas like parking garages may be exempt. Always verify local code requirements and request NFRC-certified performance data for compliance documentation.
Evaluate potential partners based on extrusion press capacity range (diverse fleets from 600T to 5500T handle any profile requirement), in-house surface treatment capabilities including anodizing and powder coating, CNC machining for precision cutting and drilling, and technical support from die development through production. Request sample profiles, material certifications, reference projects, clear pricing breakdowns, and written lead time commitments. Companies like Shengxin Aluminium with 35 extrusion presses and integrated finishing capabilities offer end-to-end accountability and factory-direct pricing.


 Интернет Сервис
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 русский
 English
 français
 Deutsch
 español
 português
 العربية
 ไทย
 Việt
 Українська