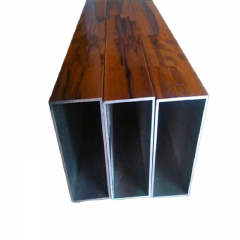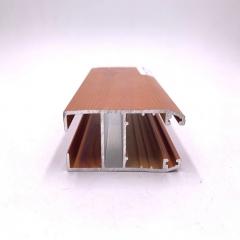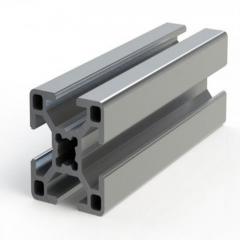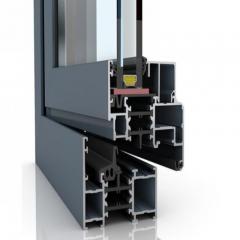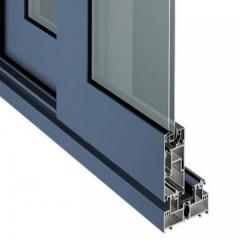
Ever wondered how companies create custom aluminum extrusion profiles without committing to massive production volumes? The answer lies in short run aluminum extrusions - a manufacturing approach that bridges the gap between one-off prototypes and full-scale mass production. Yet despite its growing importance, the industry rarely defines what "short run" actually means in concrete terms.
Short run aluminum extrusions refer to custom-manufactured aluminum profiles produced in limited quantities, typically ranging from 1 to 5,000 pieces, using customer-specific dies and tooling designed for lower-volume production economics.
When you're exploring custom aluminum extrusions, understanding quantity classifications helps you communicate effectively with suppliers and budget accurately for your project. The industry generally recognizes these distinct production tiers:
These ranges aren't arbitrary - they reflect real economic thresholds where tooling costs, setup expenses, and material minimums create natural breakpoints in pricing and production strategies.
Imagine you've developed a new product design. You might first create prototype aluminum extrusions - perhaps just 5 to 20 pieces - to validate your concept and test functionality. These prototypes often use simplified tooling or even machined samples rather than true extrusion dies.
Short run production represents the next phase. You've validated your design and now need enough units for pilot programs, initial customer shipments, or specialized applications. Unlike prototyping, this stage uses production-grade dies capable of delivering consistent aluminum extrusion profiles across every piece.
The key characteristics that define short run extrusion projects include:
This manufacturing approach has become increasingly vital for product development cycles, custom applications in specialized industries, and companies seeking to minimize inventory while maintaining supply flexibility. Whether you're developing medical devices, architectural components, or industrial equipment, understanding these distinctions helps you choose the right production path for your specific needs.
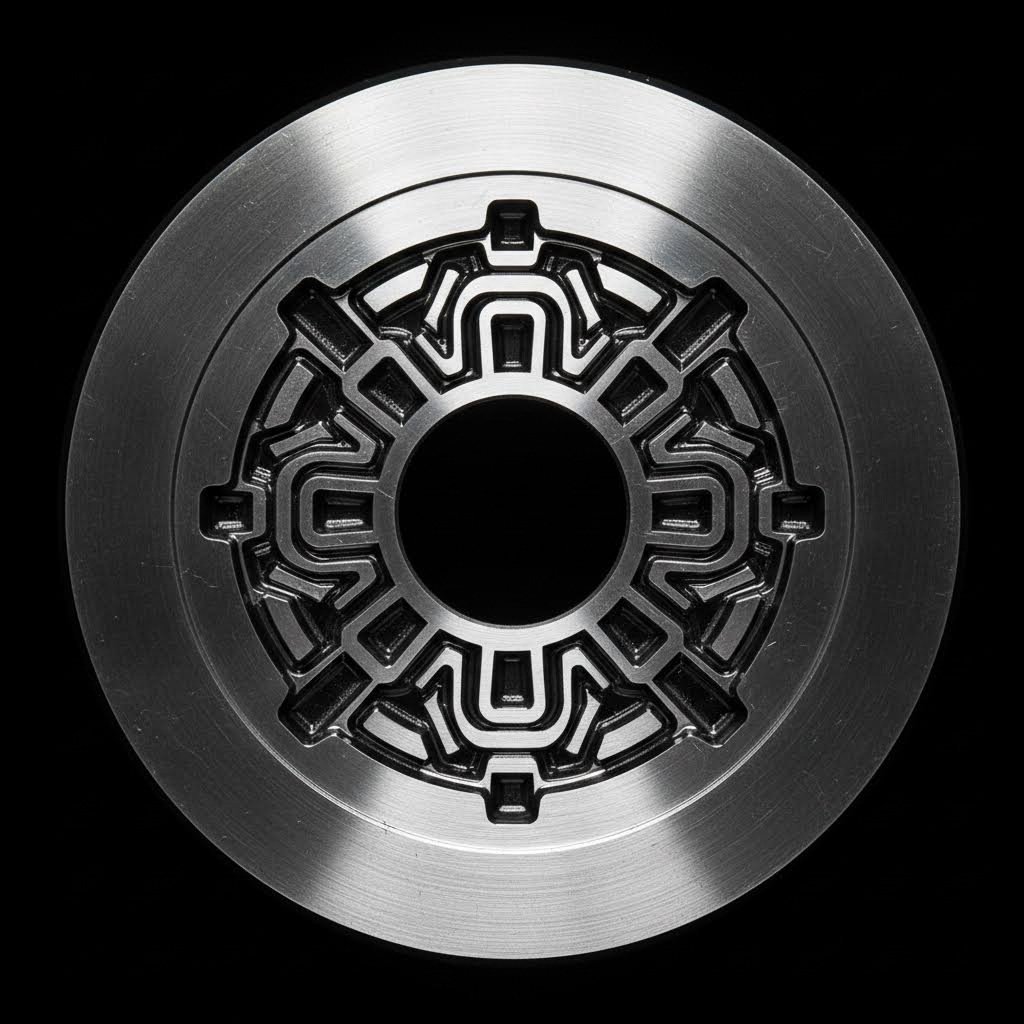
So you've determined that short run aluminum extrusion fits your project requirements. Now comes the question that often catches buyers off guard: what about the die? Unlike off-the-shelf profiles, custom extrusion requires dedicated tooling - and understanding this investment is crucial for making informed decisions about your project economics.
An aluminium extrusion die is essentially a precision-machined steel disk containing an opening that shapes the aluminum as it's forced through under immense pressure - sometimes up to 15,000 tons. For context, that's enough force to crush 50 pickup trucks simultaneously. This extreme environment demands robust engineering regardless of whether you're producing 100 pieces or 100,000.
The die development process for short run projects typically follows these phases:
For profile custom extrusions, this entire process typically spans 2-4 weeks for simple solid dies, extending to 4-6 weeks for complex hollow sections with internal cavities.
Here's where the economics get interesting. A custom extrusion aluminum project requires upfront die investment that must be amortized across your production quantity. The key question becomes: at what point does this investment make financial sense?
| Die Complexity Level | Typical Cost Range | Lead Time | Expected Lifespan | Reusability Factor |
|---|---|---|---|---|
| Simple solid profiles | $500 - $1,500 | 2-3 weeks | 50,000+ lbs of aluminum | Excellent - multiple production runs |
| Complex solid profiles | $1,500 - $3,000 | 3-4 weeks | 30,000-50,000 lbs | Very good with proper maintenance |
| Semi-hollow sections | $2,500 - $5,000 | 4-5 weeks | 25,000-40,000 lbs | Good - requires periodic refurbishment |
| Hollow/complex multi-void | $4,000 - $10,000+ | 5-6 weeks | 20,000-35,000 lbs | Moderate - higher maintenance needs |
Die ownership policies vary significantly among suppliers. Most profile custom extrusion company partners retain die ownership but store your tooling at no charge for future orders. Some offer die purchase options, giving you flexibility to move production if needed. Always clarify these terms upfront - they directly impact your long-term manufacturing strategy.
When does custom tooling make economic sense? Consider these decision factors:
Smart strategies for minimizing tooling costs include designing profiles with uniform wall thicknesses, avoiding extremely thin sections that accelerate die wear, and consolidating similar profiles where a single die might serve multiple applications. Working with experienced engineers during the design phase often identifies cost-saving opportunities that preserve your functional requirements while simplifying the aluminium extrusion dies needed for production.
You've designed your aluminum profile and understood the tooling investment. But here's a question that often gets overlooked until it's too late: which aluminum alloy should you actually use? This decision affects everything from how smoothly your parts extrude to how long your die lasts - and for short run projects, making the wrong choice can significantly impact your per-piece economics.
When it comes to extruded aluminum profiles, two alloys dominate the conversation: 6063 and 6061. Both belong to the 6000 series family, meaning they're alloyed primarily with magnesium and silicon. But don't let this similarity fool you - their performance characteristics differ significantly in ways that matter for your project.
6063 aluminum is often called the "architectural alloy" for good reason. According to Howard Precision Metals, it's the most popular extruded aluminum alloy for thin-wall and architectural applications. Why? It flows through dies like butter, produces exceptional surface finishes, and responds beautifully to anodizing. For short run aluminum extrusions where appearance matters, 6063 often emerges as the clear winner.
6061 aluminum takes a different approach. It sacrifices some extrudability for significantly higher strength - making it the go-to choice when structural performance trumps aesthetics. This alloy handles machining operations better and offers excellent corrosion resistance, which explains its popularity in aerospace, automotive, and structural applications.
| Property | 6063 Aluminum | 6061 Aluminum |
|---|---|---|
| Extrudability Rating | Excellent - flows easily through complex dies | Good - requires higher pressure and temperature |
| Tensile Strength (T6 temper) | ~30,000 psi | ~45,000 psi |
| Surface Finish Quality | Superior - ideal for decorative applications | Good - may show minor surface variations |
| Anodizing Response | Excellent - consistent, attractive finishes | Good - slightly less uniform coloring |
| Machinability | Fair | Good - easier secondary machining |
| Die Wear Impact | Lower - gentler on tooling | Higher - increases die maintenance needs |
| Typical Applications | Window frames, trim, furniture, decorative profiles | Structural components, aircraft parts, manifolds |
Sounds complex? Let's simplify the decision. Ask yourself these questions:
Here's an insight from real-world production: experienced extruders note that using 6061 for architectural trims often produces visible surface blemishes unless the die is specially polished and extrusion conditions are precisely optimized. Conversely, pushing high-strength alloys through dies designed for 6063 accelerates wear and compromises profile geometry.
For most short run aluminum profile projects, consider this practical guidance:
One final consideration: your alloy choice should be communicated early to your extrusion supplier. The die design, press parameters, and temperature controls all require adjustment based on which alloy you select. Making this decision during the design review phase - rather than after tooling is complete - ensures your aluminum extrusion shapes emerge with optimal quality and your tooling investment delivers maximum value across your production run.
You've selected your alloy, understood the tooling investment, and finalized your design. Now comes the question every project manager asks: how long until parts arrive at your dock? Surprisingly, most aluminum extrusion companies leave buyers guessing about realistic timelines. Let's fix that with a transparent breakdown of what actually happens between submitting your design and receiving finished profiles.
Short run aluminum extrusion projects move through distinct phases, each with its own timing variables. Understanding this sequence helps you plan backwards from your deadline and identify opportunities to compress the schedule.
Adding these phases together, most short run projects span 4-8 weeks from design submission to delivery. However, experienced aluminum extrusion suppliers with streamlined processes can compress this timeline significantly. Some extrusion services now advertise 2-3 week delivery for complete custom projects - roughly half the industry standard - by maintaining in-house capabilities across all production phases.
Why do similar projects sometimes finish weeks apart? Several variables create timeline differences that savvy buyers learn to anticipate and control.
Design complexity influences nearly every phase. Intricate profiles with tight tolerances require more careful die engineering, extended sample approval cycles, and additional quality checkpoints. According to manufacturing experts, complex designs for high-density heat sinks or precision parts with demanding specifications can significantly extend production timelines beyond standard estimates.
Communication clarity determines how quickly decisions move forward. Providing complete specifications upfront - including tolerances, alloy requirements, finish expectations, and quantity needs - eliminates the delays caused by information requests and clarification cycles.
Supplier capacity matters more than many buyers realize. Profile extrusion company partners with diverse press sizes and integrated finishing capabilities can often accommodate rush orders more flexibly than shops running at maximum capacity. During peak seasons, scheduling constraints may add weeks to quoted lead times.
Aluminum extrusion supply chain factors occasionally introduce unexpected delays. Alloy availability, especially for less common compositions, may require additional sourcing time. Establishing relationships with suppliers who maintain robust material inventories helps insulate your project from upstream disruptions.
Want to minimize your project timeline? Consider these practical preparations:
The aluminum extrusion supply process rewards preparation and clear communication. Projects that drag on for months typically suffer from incomplete specifications, slow approval cycles, or repeated design changes - all factors within the buyer's control. By understanding each phase and preparing accordingly, you'll find that even custom short run orders can move from concept to delivery faster than you might expect.
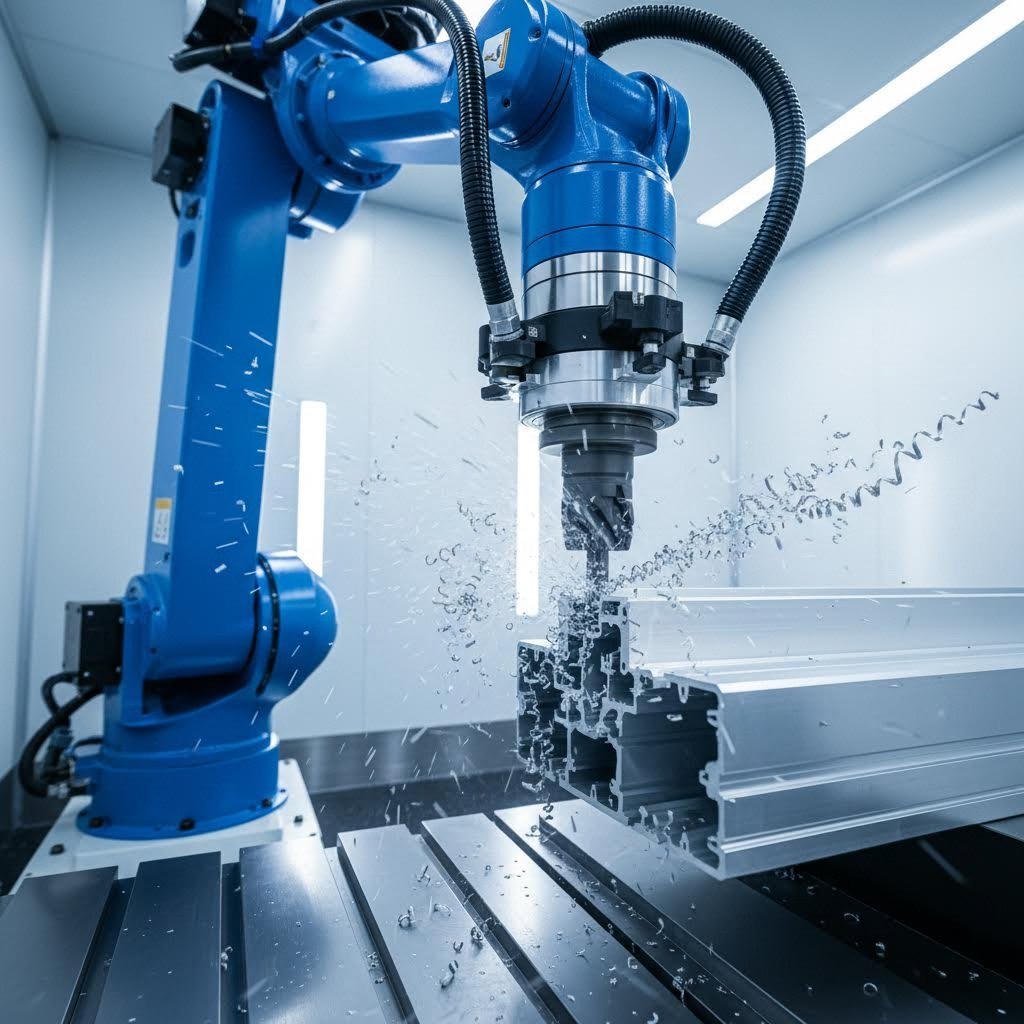
Your extruded profiles have emerged from the press with the perfect cross-section. But here's something many first-time buyers don't realize: that raw extrusion is rarely the finished product. The real magic happens in secondary operations - the machining, finishing, and fabrication steps that transform a basic aluminum shape into a ready-to-install component. For short run aluminum extrusions, these value-added services often determine whether your project succeeds economically.
Think of secondary operations as the bridge between extrusion and assembly. According to industry manufacturing data, most extruded profiles require additional machining such as drilling, milling, and tapping to meet final part features and tolerances. These operations add functionality that extrusion alone cannot deliver directly.
Common secondary operations for aluminum extrusion parts include:
For extruded aluminum trim profiles used in architectural applications, secondary operations often include mitering for corner joints, notching for overlapping connections, and precision hole patterns for mounting hardware. Similarly, aluminium extrusion trim for automotive interiors typically requires close-tolerance machining to ensure perfect fit within vehicle assemblies.
Here's where short run production really shines. CNC aluminium extrusion machining creates hybrid manufacturing solutions that deliver complex parts at costs impossible to achieve through machining alone. Why? Because extrusion provides the basic shape economically, while CNC operations add only the features that require precision machining.
Consider this perspective from manufacturing experts: even if the base extrusion is identical, different customers can receive customized variants through simple post-machining. This approach saves cost, simplifies inventory, and improves flexibility - exactly what short run projects demand.
What makes CNC machining particularly powerful for machined aluminum extrusion projects?
The economics work especially well for short runs because you're not paying for extensive stock removal. Your profile already contains most of the material in its final configuration. CNC simply adds the finishing touches - often reducing machining time by 60-80% compared to starting from solid bar stock.
Beyond dimensional modifications, surface treatments transform both the appearance and durability of your extruded aluminum trim and components. According to Aluminum Extruders Council research, selecting the right finish is critical to application success - and the options extend far beyond basic mill finish.
Anodizing remains the most popular finish for aluminum extrusions requiring corrosion resistance and aesthetic appeal. This electrochemical process creates a hard oxide layer that's integral to the aluminum surface. Clear anodizing preserves the natural metal appearance, while electrolytic coloring produces consistent gray, bronze, and black tones with excellent light resistance. For short run architectural components, anodizing delivers durability that outperforms paint in many environments.
Powder coating offers virtually unlimited color options with excellent durability. Modern vertical powder coating lines, as noted in industry presentations, increasingly incorporate automation for consistent quality and reduced labor requirements. For short run projects requiring specific brand colors or multi-color designs, powder coating provides flexibility that anodizing cannot match.
Specialty finishes address specific performance requirements:
One important consideration: your surface treatment choice should be decided early in the project. Some finishes require specific alloy compositions for optimal results. For instance, research indicates that the temper of aluminum significantly affects anodizing quality - T4, T5, T6, and T52 tempers each produce different results in coating weight density and appearance consistency.
For short run aluminum extrusion parts, partnering with suppliers offering integrated secondary operations and finishing eliminates coordination headaches and reduces total lead time. Rather than shipping profiles between multiple vendors, one-stop processing keeps your project moving efficiently toward final delivery.
Here's something most aluminum extrusion suppliers won't tell you: custom extrusion isn't always the right answer. Sometimes machining from bar stock makes more sense. Occasionally, 3D printing delivers better value. And for certain applications, stock aluminum extrusions from standard catalogs solve your problem faster and cheaper than any custom approach. Knowing when to choose alternatives saves you money, time, and frustration.
Custom extrusion shines in specific scenarios - but falls short in others. Understanding the decision criteria helps you match your manufacturing method to your actual requirements rather than forcing a solution that doesn't fit.
Machining from bar stock often wins when:
According to manufacturing analysis from Thunderbird Metals, machining begins with a larger amount of material than the finished part and requires "hogging out" of material to achieve the finished geometry. This approach wastes material and burns through time and tooling - but for very low quantities, it remains faster and more economical than custom die development.
3D printing (additive manufacturing) makes sense when:
Off-the-shelf extruded shapes deserve consideration when:
The Aluminum Extruders Council notes that most extruders have minimum order sizes, often 1,000 to 2,000 pounds per shape. When your aluminum extrusion projects require quantities well below these thresholds, alternatives often prove more practical.
Making the right manufacturing choice requires honest comparison across multiple factors. The following table breaks down how each approach performs in the criteria that matter most for short run production:
| Manufacturing Method | Ideal Quantity Range | Complexity Capability | Typical Lead Time | Relative Cost Structure |
|---|---|---|---|---|
| Custom Short Run Extrusion | 100-5,000 pieces | Excellent for 2D cross-sections; limited 3D features | 4-8 weeks (includes die development) | High upfront tooling; low per-piece cost |
| CNC Machining from Bar Stock | 1-500 pieces | Excellent for complex 3D geometries | 1-3 weeks | No tooling; high per-piece cost |
| 3D Printing (Metal) | 1-50 pieces | Exceptional - nearly unlimited geometry | 1-2 weeks | Very high per-piece; no tooling |
| Stock Extrusion Shapes | Any quantity | Limited to catalog profiles | Days (from inventory) | Lowest cost for standard shapes |
| Impact Extrusion | 1,000-100,000+ pieces | Good for cylindrical/tubular shapes | 4-6 weeks | Moderate tooling; very low per-piece |
Notice how the sweet spot for custom short run extrusion falls between pure prototyping quantities and mass production volumes. Below 100 pieces, tooling investment rarely makes economic sense. Above 5,000 pieces, you're entering territory where longer production runs and volume pricing become increasingly attractive.
The decision criteria that should guide your choice:
One practical approach: request quotes for both custom extrusion and machined alternatives for the same part. When quantities fall in the gray zone between 50-200 pieces, the comparison often reveals surprising insights about which method truly delivers better value for your specific geometry and requirements.
The honest truth? Custom extrusion represents the optimal choice for many short run applications - but not all. Recognizing when alternatives serve you better demonstrates manufacturing sophistication and often leads to faster, more cost-effective project outcomes. With this understanding of your options, you're now ready to explore how different industries leverage short run capabilities for their specialized applications.
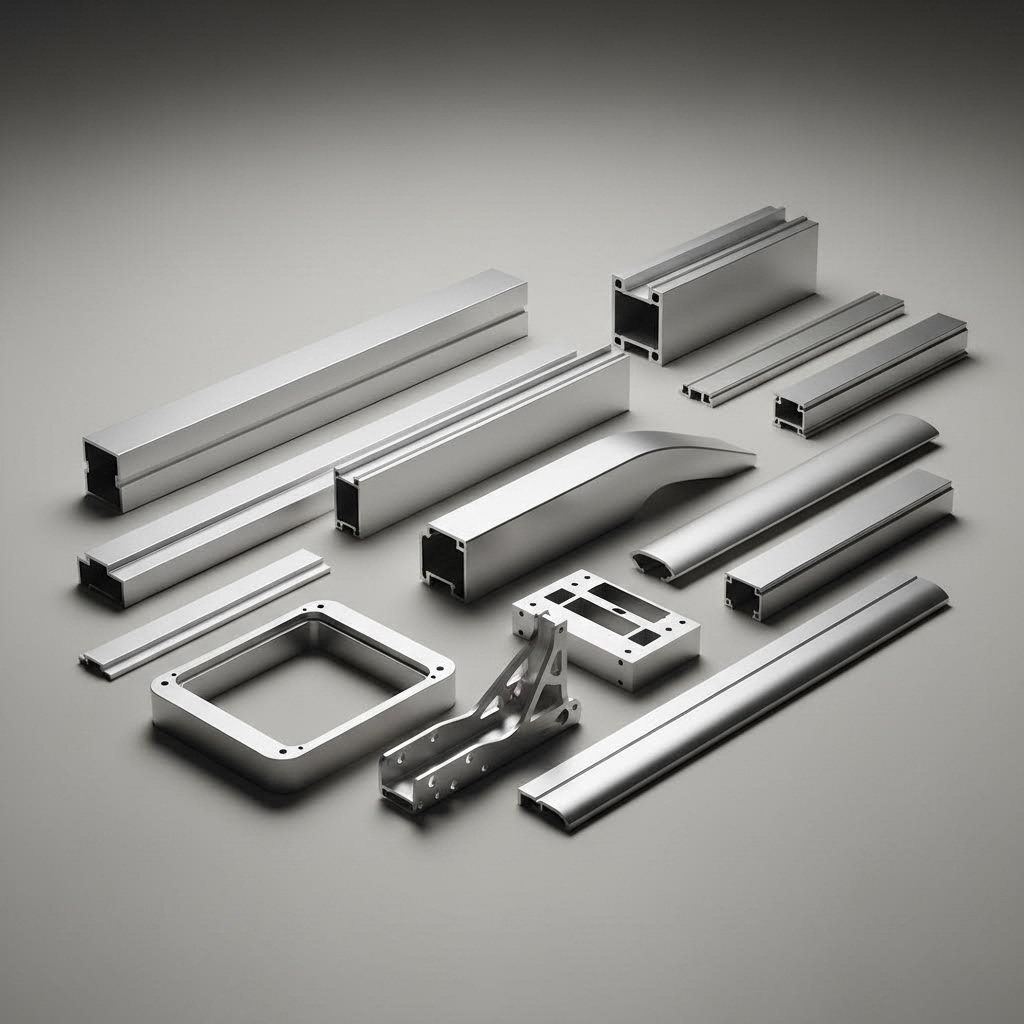
Now that you understand when short run extrusion makes sense compared to alternatives, let's explore where these capabilities deliver the most value. Across diverse industries, companies rely on custom aluminum products manufactured in limited quantities - not because they can't afford larger runs, but because their applications genuinely require it. From operating rooms to aircraft cabins, short run aluminum extrusions solve problems that mass production simply cannot address.
Different sectors turn to short run production for vastly different reasons. Some need specialized geometries that serve niche markets. Others face regulatory hurdles requiring extensive validation before scaling up. Still others use limited runs for market testing before committing to full production tooling investments.
Medical Devices and Healthcare Equipment
The medical industry represents one of the most demanding environments for aluminum extrusion profile applications. According to Medical Design Briefs, OEMs are increasingly turning to aluminum extrusions instead of more costly materials to control product development costs without sacrificing quality.
Why short runs specifically? Medical device manufacturers face unique challenges. As industry experts note, even the slightest change in process or design variation can potentially require revalidation, increasing costs and delaying time to market. Short run capabilities allow iterative development while maintaining regulatory compliance throughout the validation process.
Aerospace Components
Aerospace applications demand aluminium extrusion parts that meet extraordinarily stringent requirements. AS9100 certification - the quality management standard for aviation, space, and defense organizations - represents the baseline expectation for suppliers serving this sector.
Short run production serves aerospace particularly well because aircraft programs often require limited quantities of highly specialized components. A curved aluminum extrusion for a business jet interior might need only 200-500 pieces annually - quantities where custom tooling investment makes sense but mass production volumes never materialize.
Architectural and Construction Elements
Architects and designers increasingly specify custom profiles for distinctive building features that standard catalog shapes cannot achieve.
Industrial Equipment and Machinery
Manufacturing environments rely on custom aluminum extrusion profiles for equipment frames, guarding systems, and material handling components.
Consumer Products and Electronics
Product developers leverage short runs for market testing before committing to high-volume production tooling.
What makes short run capabilities essential across these diverse applications? The answer varies by industry, but common threads emerge.
For medical applications, surface cosmetics rank among the top factors when specifying aluminum extrusion services. With proper finishing treatments such as anodizing, aluminum extruded products can actually be less porous and cleaner than stainless steel - a critical consideration for preventing contamination in medical care environments.
Aerospace demands traceability and documentation that accompanies every aluminium extrusion parts shipment. Material certifications, process records, and dimensional inspection reports ensure compliance with airworthiness requirements. Short run suppliers serving this sector maintain rigorous quality systems that larger commodity producers often cannot justify for limited quantity orders.
Architectural applications prioritize finish consistency across potentially years-long project timelines. A building facade installed in phases requires matching profiles regardless of when each batch was extruded. Suppliers capable of maintaining die condition and finish standards across intermittent short runs deliver value that goes beyond simple manufacturing.
As manufacturing trends indicate, devices across industries are shrinking in size and weight to enhance portability, mobility, and handling. This transformation pushes OEMs toward aluminum extrusions with smaller profiles to cut material costs while maintaining strength - a perfect application for short run production capabilities that allow design optimization without massive volume commitments.
Whether your project involves unique extrusions for specialized equipment or profile precision extrusions for demanding applications, understanding how your industry peers leverage short run capabilities helps frame your own manufacturing decisions. The key lies in matching production approach to actual requirements - not defaulting to mass production economics when your application truly demands something more tailored.
You've identified your application requirements, selected an alloy, and explored secondary processing options. Now comes a decision that will shape your entire project experience: which supplier should you trust with your short run aluminum extrusions? Unlike commodity purchases where price dominates, custom aluminum extruders require evaluation across multiple dimensions that directly impact your final product quality, timeline, and total cost of ownership.
Finding certified aluminum suppliers for custom products demands more than comparing quotes. According to industry sourcing experts, a qualified aluminum extrusion supplier offers much more than extruded profiles - they provide engineering collaboration, quality assurance, and integrated production capabilities that align with your business goals.
When evaluating potential custom aluminum extrusions suppliers, assess these essential factors:
One often-overlooked criterion: financial stability. A growth-oriented supplier invests in technology, maintains quality consistency, and honors long-term commitments. Reviewing business credentials and expansion history protects your supply chain from sudden disruptions.
Beyond basic capabilities, the best aluminum extrusion services function as true manufacturing partners - extending your own production team rather than simply fulfilling orders. What separates adequate suppliers from exceptional ones?
End-to-end support from die development to finished parts
Top aluminum suppliers for custom products guide you through every phase: design optimization, die engineering, sample approval, production, finishing, and logistics. This comprehensive approach reduces your coordination burden and ensures accountability at each step. For example, Shengxin Aluminium exemplifies this integrated model with over 30 years of industry experience, operating 35 extrusion presses ranging from 600T to 5500T capacity, paired with CNC machining centers and comprehensive aluminum profile processing capabilities for secondary operations.
Surface treatment versatility
Your project requirements may evolve, and partnering with suppliers offering diverse finishing options provides flexibility. Look for capabilities including:
Practical verification steps before commitment
Before finalizing your supplier selection, take these validation steps recommended by custom extruded aluminum specialists:
When you partner with aluminum extrusion suppliers who demonstrate these qualities, your short run projects benefit from accumulated expertise that prevents costly mistakes. Industry experience confirms that choosing a manufacturer based solely on price or speed without verifying technical capability often leads to subpar products, delays, and escalating costs.
Warning signs to watch for
Be cautious of suppliers who:
The right manufacturing partner transforms short run projects from stressful procurement exercises into collaborative successes. With supplier evaluation criteria established, you're now ready to prepare your own project documentation - the final step before production begins.
You've evaluated suppliers, understood the economics, and confirmed that custom profile extrusion fits your application. Now comes the moment where preparation meets production. The steps you take before submitting your order directly determine whether your aluminum extrusion custom project flows smoothly or encounters preventable delays. Let's walk through exactly how to set your project up for success.
Your design files serve as the foundation for everything that follows - die development, sample approval, and production quality. According to Howard Precision Metals, providing the desired shape in a CAD software file like .DWG or .DXF ensures dimensional measurements are accurate and allows for ease in quoting your finished shape.
Follow this sequence to prepare production-ready documentation:
One often-missed preparation step: understanding the manufacturing processes that follow extrusion. As experienced distributors warn, many cutoff saws have pneumatic hold down clamps that can put too much pressure on thin walls and potentially crush the metal. Communicating your downstream operations helps engineers design profiles that survive secondary processing.
For custom aluminium extrusion projects where tooling investment matters, smart design choices reduce die complexity and extend tool life. These principles help you achieve functional requirements while keeping aluminum extrusion cost under control:
Even experienced buyers make preventable errors that delay projects and inflate costs. Here's what to watch for:
Over-specifying tolerances
Requesting tighter tolerances than your application actually requires increases die cost, extends sample approval cycles, and raises rejection rates. Industry guides identify over-specifying dimensional tolerances and incorrectly notating tolerances among the most common design issues. Ask yourself: does this dimension truly need ±0.005 inches, or will standard ±0.012 inches work?
Incomplete specifications
Missing information triggers email exchanges that add days or weeks to your timeline. Manufacturers consistently report that lack of proper information and product requirements causes significant project delays. Provide complete requirements upfront rather than answering questions piecemeal.
Ignoring alloy-finish compatibility
Specifying an alloy that performs poorly with your intended finish creates problems discovered only after extrusion. If you need consistent anodized color, 6063 outperforms 6061. If you need strength plus coating, verify compatibility before finalizing your material selection.
Slow sample approval responses
Your supplier produces samples and waits for your approval. Every day you delay reviewing samples adds directly to your delivery timeline. Establish internal review processes before samples arrive so you can respond within 24-48 hours.
Last-minute design changes
Modifying profiles after die fabrication begins often requires starting tooling over - doubling both cost and lead time. Invest adequate time in design validation before authorizing die production.
Clear communication prevents misunderstandings that derail custom profile extrusions projects. Industry veterans emphasize that clear communication with suppliers is essential for ensuring products meet required specifications.
Establish these practices from project inception:
Suppliers like Shengxin Aluminium provide technical team support from die development through mass production, offering guidance that helps first-time buyers navigate the custom extrusions process successfully. Their factory-direct pricing for custom 6063 aluminum tubes, architectural profiles, and industrial components reflects over 30 years of experience translating customer requirements into production-ready specifications.
Ready to move forward with your aluminum extruded project? Start by gathering your CAD files, defining your critical tolerances, and documenting your finish requirements. With proper preparation, your short run production will progress from design approval to delivery with minimal friction - delivering custom profiles that meet your exact specifications at costs that make economic sense for your quantity requirements.
For those prepared to explore custom extrusion services with comprehensive processing capabilities, Shengxin Aluminium's deep processing services offer integrated solutions from initial die design through finished, ready-to-install components.
Short run aluminum extrusions typically range from 1 to 5,000 pieces. True short runs fall between 1-500 pieces for specialized applications, while low-volume production spans 500-5,000 pieces for established products with limited demand. These ranges reflect economic thresholds where tooling costs, setup expenses, and material minimums create natural pricing breakpoints.
Custom die costs vary by complexity. Simple solid profiles range from $500-$1,500 with 2-3 week lead times. Complex solid profiles cost $1,500-$3,000. Semi-hollow sections run $2,500-$5,000, while hollow multi-void dies can exceed $10,000. Dies typically last 20,000-50,000+ pounds of aluminum production with proper maintenance and storage.
Most short run projects span 4-8 weeks from design submission to delivery. This includes design review (3-7 days), die development (7-17 days), sample production (5-14 days), production extrusion (3-7 days), finishing operations (5-10 days), and shipping (3-7 days). Experienced suppliers like Shengxin Aluminium with 35 extrusion presses can compress timelines through integrated capabilities.
Choose 6063 for applications requiring excellent surface finish, anodizing quality, thin walls, or when maximizing die longevity matters. Select 6061 when structural strength is paramount, extensive CNC machining follows extrusion, or higher mechanical properties are needed. 6063 offers better extrudability while 6061 provides approximately 50% higher tensile strength.
Consider CNC machining from bar stock for quantities below 50-100 pieces, extremely tight tolerances, or complex 3D geometries. Use 3D printing for 1-20 prototype pieces with impossible-to-extrude features. Choose stock extrusion shapes when standard profiles meet requirements with minor modifications. Custom extrusion becomes cost-effective typically above 100 pieces for uniform cross-sections.


 Интернет Сервис
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 русский
 English
 français
 Deutsch
 español
 português
 العربية
 ไทย
 Việt
 Українська