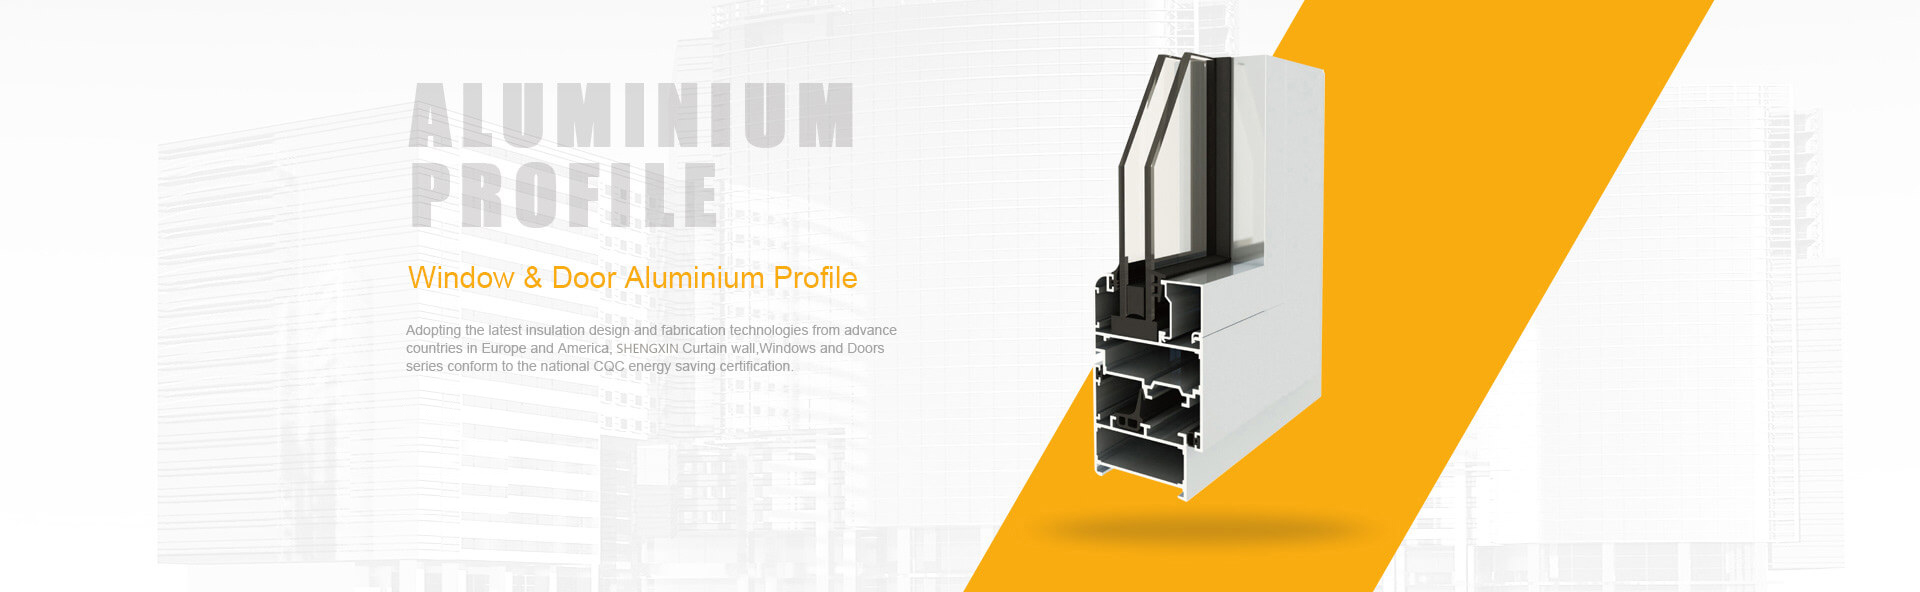
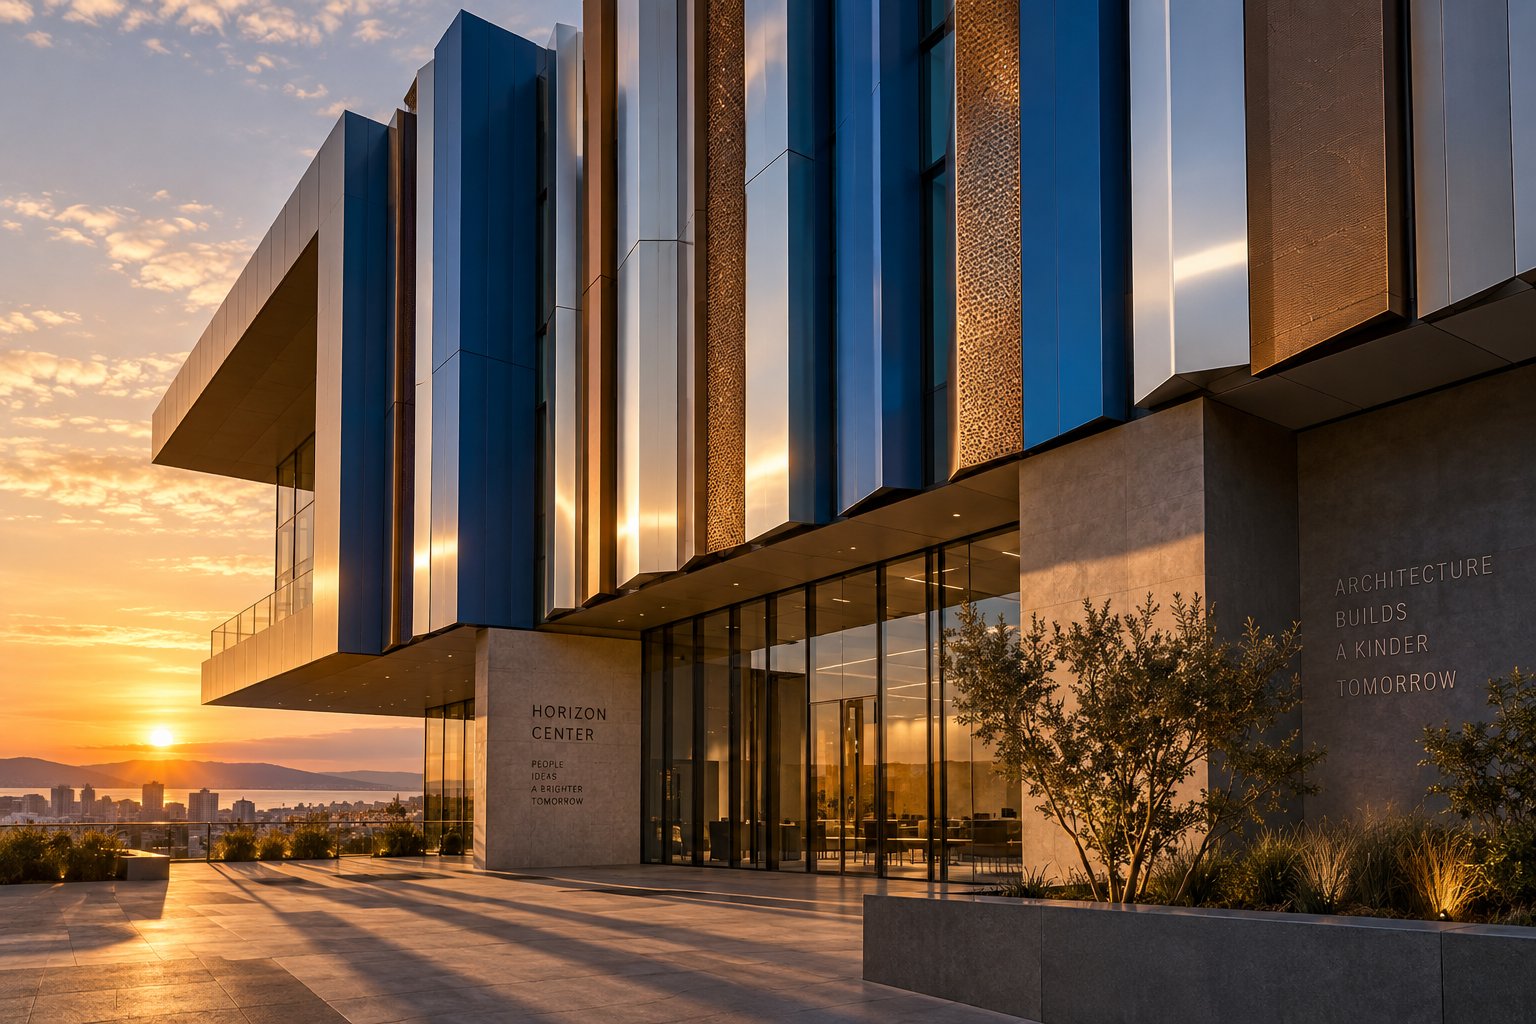
Have you ever wondered what gives modern buildings their sleek, colorful facades or how outdoor equipment maintains its vibrant appearance year after year? The answer often lies in painted aluminum extrusions. These versatile components combine the lightweight strength of aluminum extruded profiles with protective and decorative paint finishes, creating products that perform as beautifully as they look.
So, what is aluminum extrusion exactly? It's a manufacturing process where aluminum alloy is forced through a shaped die to create profiles with consistent cross-sections. When these extrusions receive a painted finish, they gain an additional layer of protection and aesthetic appeal that raw aluminum simply cannot match.
Unlike raw or anodized metal extrusions, painted versions offer something unique: unlimited color possibilities combined with enhanced environmental protection. The global aluminum extrusion market reached a projected value of over USD 90 billion in 2022, with painted finishes representing a significant portion of this demand.
The distinction comes down to the finishing process itself. Extrusions aluminum profiles can receive either liquid coatings or powder coatings, each following strict industry specifications set by the American Architectural Manufacturers Association (AAMA). These standards ensure consistent quality across applications ranging from architectural curtain walls to industrial equipment housings.
Surface finishing transforms aluminum from a functional material into a long-lasting, visually striking component. Without proper coating protection, even the most precisely manufactured extrusion remains vulnerable to environmental degradation, UV damage, and aesthetic deterioration over time.
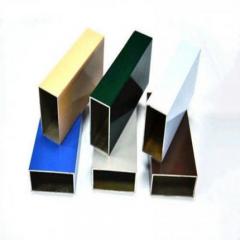
Painted extrusions serve dual purposes that make them indispensable across industries. From an aesthetic standpoint, they offer virtually any color imaginable through polyesters, acrylics, siliconized polyesters, and fluoropolymers. On the protective side, these coatings shield the underlying aluminum from corrosion, UV exposure, and physical wear.
The building and construction industry currently utilizes the largest share of extruded aluminum products. Architectural elements like engineered skylights, canopies, and window frames demand both structural integrity and visual appeal. This is precisely where painted finishes excel.
Throughout this guide, you'll discover everything from painting processes and AAMA specifications to color matching and ordering strategies. Whether you're an architect specifying finishes for a new project, an engineer evaluating material options, or a procurement professional navigating supplier selection, this resource provides the technical foundation you need for informed decision-making.
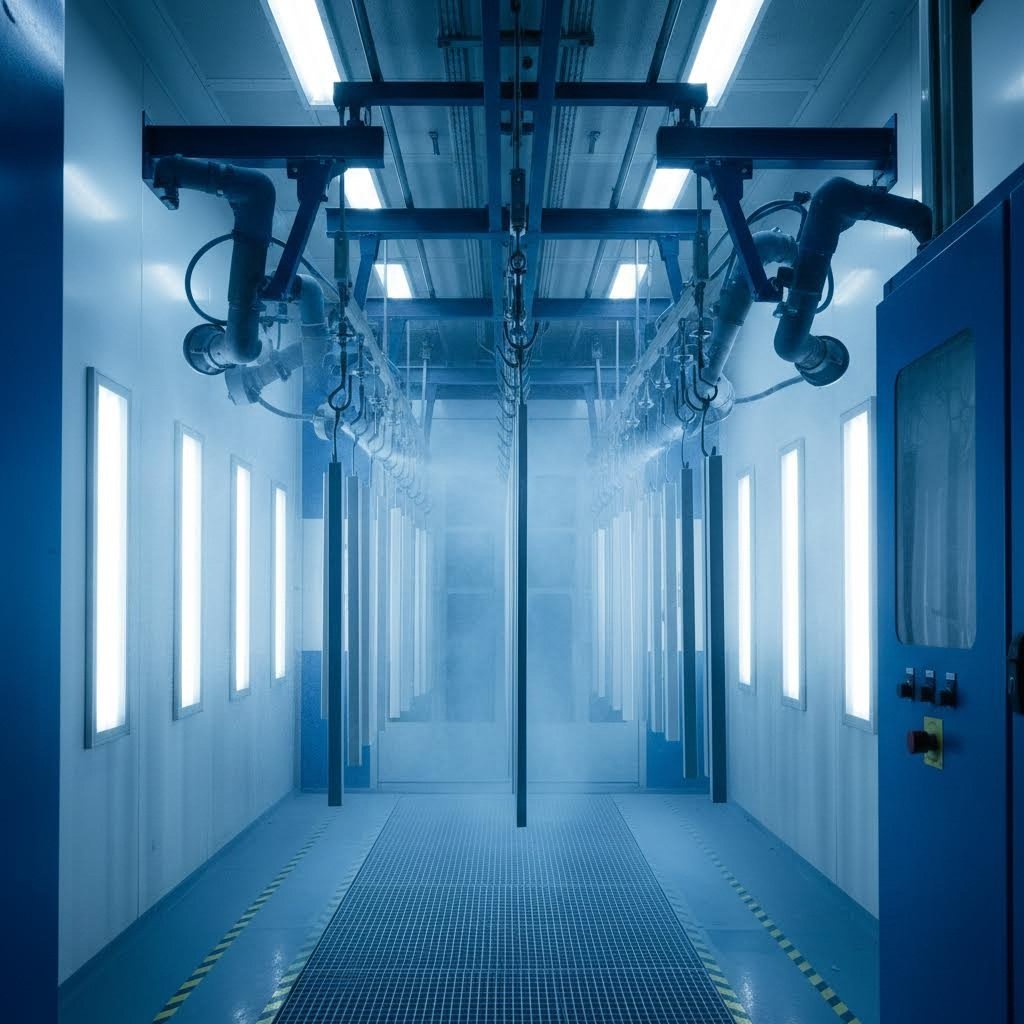
Before any color touches an extruded aluminum channel, there's a critical question every manufacturer must answer: which painting method delivers the best results for the application? The answer depends on durability requirements, finish preferences, and budget considerations. Let's break down the three primary methods used to transform standard aluminum extrusions into vibrant, protected components.
Powder coating has become the most influential finishing method for aluminum channel extrusions in recent decades. But how does it actually work?
Imagine tiny particles of dry powder—containing resins, pigments, and additives—being electrostatically charged and sprayed onto a grounded aluminum profile. The positive charge on the powder particles creates an attraction to the negatively charged metal surface, causing them to cling uniformly before any heat is applied.
Here's where the transformation happens: the coated profile enters a curing oven where temperatures typically reach 350-400°F. The powder particles melt into a liquid state, fuse together, and form a continuous, homogenous film. This thermal curing process creates a finish that's significantly more durable than many liquid alternatives.
Why has powder coating gained such popularity? According to Alexandria Industries, it's one of the lowest-cost finishing methods available today. While material and equipment costs remain comparable to liquid systems, substantial savings emerge in energy consumption, labor efficiency, waste disposal, and regulatory compliance. Since powder coatings contain virtually no volatile organic compounds (VOCs), manufacturers avoid many environmental compliance costs that burden solvent-based alternatives.
Liquid coatings take a different approach to protecting extruded metal surfaces. These fluid materials consist of three primary components: pigments for color, binders for adhesion, and solvents that enable application before evaporating during the cure cycle.
You'll notice that liquid coatings are classified by their volume solids content—the percentage of material that remains on the surface after solvents evaporate. Higher solids formulations leave thicker films, while lower solids versions require multiple coats to achieve adequate protection.
When does liquid coating outperform powder? For projects requiring exceptionally thin, uniform films with glass-smooth finishes, liquid application often delivers superior results. This makes it particularly valuable for decorative projects where aesthetic perfection takes priority.
Electrostatic spray techniques enhance both powder and liquid application by ensuring uniform coverage on complex aluminum extrusion profiles. The electrostatic charge wraps coating particles around edges and into recesses that conventional spray methods might miss. For intricate extruded aluminium channel profiles with multiple surfaces and angles, this technology proves invaluable.
Here's a reality many overlook: even the finest coating will fail without proper surface preparation. Aluminum is naturally non-porous and smooth, which sounds advantageous but actually creates adhesion challenges.
The preparation sequence typically includes:
When considering how to cut aluminum extrusion or how to cut extruded aluminum for a project, remember that any cut edges will need the same preparation treatment as the original profile surfaces before painting can occur.
| Criteria | Powder Coating | Liquid Coating | Electrostatic Spray |
|---|---|---|---|
| Application Process | Electrostatic spray of dry powder by thermal curing at 350-400°F | Wet spray application with solvent evaporation during baking | Charged particle application (works with both powder and liquid) |
| Finish Quality | Excellent uniformity; slightly textured appearance possible | Superior smoothness; thin, uniform film thickness | Enhanced coverage on complex profiles and edges |
| Durability | Excellent impact, scratch, and chemical resistance | Good to excellent depending on formulation | Matches base coating durability with improved edge coverage |
| Cost Considerations | Lower overall cost due to reduced waste, energy, and compliance expenses | Higher material and disposal costs; VOC compliance required | Equipment investment offset by material savings |
| Best-Suited Applications | Architectural profiles, industrial equipment, outdoor furniture | Specialty decorative finishes, thin-film requirements | Complex extrusion profiles with multiple surfaces and angles |
Understanding these coating options positions you to specify the right finish for your project. But how do you ensure that finish meets recognized quality standards? That's where AAMA specifications come into play, providing measurable performance criteria that separate adequate coatings from exceptional ones.
You've selected your coating method and prepared your aluminum channels for finishing. Now comes a critical decision that will determine how your painted extrusions perform over time: which AAMA specification should you require?
Think of AAMA specifications as performance tiers for painted aluminum extrusions. Originally developed by the American Architectural Manufacturers Association (now the Fenestration and Glazing Industry Alliance), these voluntary standards establish minimum performance requirements through rigorous testing. Whether you're specifying aluminum channel dimensions for a commercial storefront or selecting finishes for industrial equipment, understanding these three specifications helps you match coating performance to project demands.
AAMA 2603 represents the entry-level specification for painted aluminum extrusions. But don't let "entry-level" mislead you—these coatings still undergo meaningful performance testing.
This specification applies to coatings less than 1 mil thickness and evaluates performance across multiple criteria including color uniformity, specular gloss, impact resistance, and chemical resistance. The weathering test—exposure in South Florida's demanding climate—is optional for this tier, with only one year of color retention and chalk resistance required.
When does AAMA 2603 make sense? Consider it for:
Standard polyester powders typically meet AAMA 2603 requirements. These coatings work well for interior uses where weathering conditions aren't a primary concern, though some manufacturers use them on low-value residential exteriors like fixtures and fittings.
Stepping up to AAMA 2604 or 2605 means significantly stricter testing requirements and longer-lasting performance guarantees. Both specifications apply to coatings greater than 1.2 mils in thickness and are intended for commercial and architectural-grade applications.
AAMA 2604: The High-Performance Middle Ground
AAMA 2604 delivers five years of color retention and chalk resistance—a substantial improvement over the basic tier. This specification requires mandatory extended South Florida exposure testing and includes additional criteria for abrasion resistance, chemical resistance, and humidity performance.
Super durable polyester powders meet AAMA 2604 requirements and typically carry 10-year warranties when applied by registered applicators to aluminum. You'll find these coatings on commercial storefronts, windows, doors, and other exterior applications where robust mid-term performance matters. For aluminum c channel sizes used in visible exterior trim or aluminum u channel sizes specified for window framing, AAMA 2604 often provides the right balance of performance and value.
AAMA 2605: Premium Architectural Performance
For projects demanding maximum durability, AAMA 2605 stands as the premium specification. This tier requires ten years of color retention and chalk resistance, with weathering testing requirements double those of AAMA 2604.
According to industry testing data, AAMA 2605 coatings demonstrate superior performance in color and gloss retention, abrasion resistance, salt spray resistance, and humidity exposure. FEVE-based fluoropolymer powders and 70% PVDF liquid coatings typically meet this specification, carrying 20-year warranties when properly applied.
Where do AAMA 2605 finishes belong? Think high-visibility, high-value projects:
Each AAMA specification addresses the same fundamental performance areas, but with progressively stricter requirements:
Matching specifications to your project environment ensures you're not overpaying for performance you don't need—or underspecifying for conditions that will degrade your finish prematurely. With the right AAMA tier selected, you're ready to explore how painted finishes compare against other aluminum surface treatments.
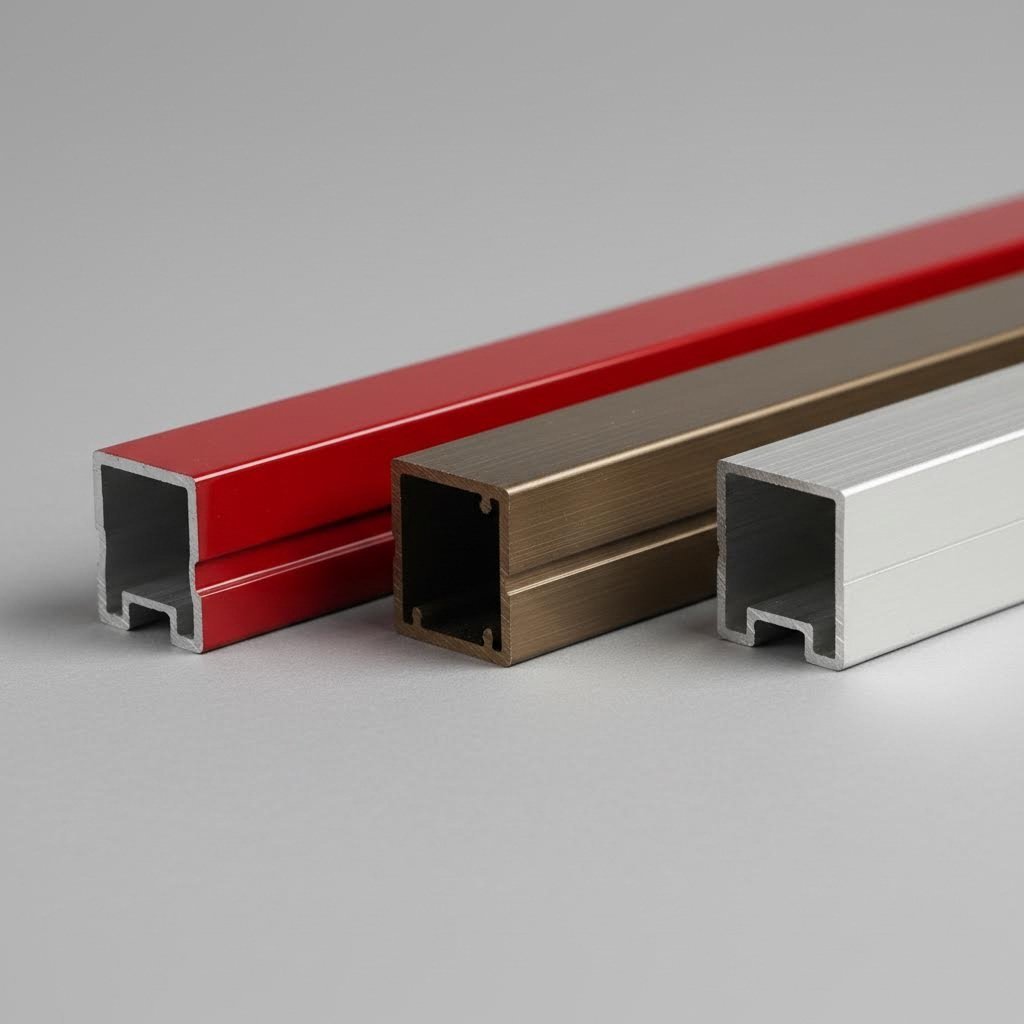
Now that you understand AAMA specifications and coating methods, you face perhaps the most fundamental question in aluminum finishing: should you paint, anodize, or leave the metal raw? Each approach offers distinct advantages, and the right choice depends on your specific project requirements, budget constraints, and aesthetic goals.
Imagine walking through a modern office building. The sleek bronze anodized aluminum tubing on the handrails feels solid and resilient under your hand. Meanwhile, the vibrant blue window frames—painted to match the company's brand colors—create a striking visual statement. Both finishes serve their purposes beautifully, but they achieve their results through fundamentally different processes.
When color matters most, painted aluminum extrusions offer something neither anodizing nor raw aluminum can match: virtually unlimited color options. According to Sherwin-Williams research, painted aluminum provides a clear advantage from a color standpoint, with options ranging from high-intensity solids to naturals, micas, and metallics.
What does this mean for your project? Whether you need to match a specific RAL code for European architectural standards or a Pantone color for brand consistency, paint can deliver. The industry-standard paint finish range is narrower than anodizing at 2 Delta E, allowing for better color matching between batches and building components.
Consider these practical advantages of painted finishes:
For aluminum u channel applications in storefronts or u channel aluminum trim on commercial buildings, painted finishes allow architects to differentiate their designs while maintaining long-term appearance. This flexibility explains why architects increasingly trend toward paint to create signature looks that complement glass, marble, and stone features.
Anodizing takes a completely different approach to finishing aluminum. Rather than applying a coating on top of the metal, this electrochemical process transforms the aluminum's surface into a hard, durable layer of aluminum oxide. The result integrates directly with the base metal—it cannot chip or peel like applied coatings.
This integral bond creates exceptional hardness. Industry experts compare anodized hardness to sapphire, making it significantly more abrasion-resistant than painted surfaces. For high-traffic areas like door stiles, kick plates, and push/pull bars on aluminium u channel frames, this durability advantage becomes critical.
When should you specify anodizing? Consider these scenarios:
Anodizing does have limitations worth understanding. Color choices remain restricted to clear, champagne, bronze, gold/silver, black, and limited blues, greens, and reds. Batch-to-batch color variation runs higher than with paint—the anodized standard is 2-3 Delta E compared to paint's tighter 2 Delta E range. Additionally, different aluminum alloys respond differently to anodizing, creating slight color variations that can compound on large projects.
Perhaps the most significant limitation? Anodizing cannot be touched up in the field. Damaged sections require complete replacement, which proves expensive compared to repainting a localized area.
Sometimes, neither painting nor anodizing makes sense. Raw aluminum—often called mill finish—serves applications where appearance takes a back seat to function and cost efficiency.
You'll find mill finish aluminum in concealed structural applications, temporary installations, and industrial settings where aesthetic concerns are minimal. The natural oxide layer that forms on exposed aluminum provides basic corrosion protection, though far less than either painted or anodized surfaces.
Raw aluminum costs less initially, but consider the tradeoffs: no UV protection, limited corrosion resistance in harsh environments, and an industrial appearance that may not suit visible applications.
| Criteria | Painted Finishes | Anodized Finishes | Raw Aluminum |
|---|---|---|---|
| Color Options | Virtually unlimited; RAL, Pantone, custom matching available | Limited palette: clear, bronze, champagne, black, select colors | Natural silver-gray mill finish only |
| Durability Factors | Excellent scratch and mar resistance; can be damaged by impact | Sapphire-like hardness; exceptional abrasion resistance | Minimal protection; prone to scratching and marking |
| UV Resistance | Excellent with PVDF coatings; 10+ years color retention (AAMA 2605) | Good with proper pigments; dyes may fade over time | None; surface will oxidize and discolor |
| Corrosion Protection | Outstanding protection against salt spray, humidity, acid rain | Good barrier protection; vulnerable to chemical attack | Basic natural oxide layer only |
| Scratch Resistance | Mar resistant but can be scratched with rough handling | Superior; very hard coating resists most abrasion | Poor; easily scratched and marked |
| Expected Lifespan | Up to 40 years with premium PVDF coatings and proper maintenance | 5-10 years typical warranty; renewable through cleaning | Variable; depends entirely on environment |
| Cost Range | Powder coating lowest; PVDF liquid higher; custom colors add cost | Lower initial cost for standard colors; specialty colors expensive | Lowest initial cost; no finishing expense |
| Ideal Applications | Curtain walls, metal roofing, custom color projects, high-traffic areas needing easy repair | Storefronts, handrails, high-abrasion areas, metallic appearance requirements | Concealed structural elements, temporary installations, industrial equipment |
Sustainability increasingly influences material decisions, and aluminum finishing is no exception. Each method carries different environmental implications worth considering.
Powder coatings contain little to no VOCs, making them environmentally favorable compared to solvent-based liquid paints. According to SAF's analysis, when powders cure in an oven, they emit no air pollution—a significant advantage as regulations tighten nationwide.
Anodizing presents a mixed environmental picture. The process emits no ozone-producing solvents and uses no heavy metals. Aluminum sulfate from anodizing effluent can actually improve settling efficiency at municipal wastewater treatment plants. However, multiple chemicals are used in the process, and thick anodizing requires more electrical energy than coating processes.
Both finishes extend aluminum's already impressive sustainability profile. Aluminum is infinitely recyclable without losing properties, and properly finished aluminum lasts decades—reducing replacement cycles and associated resource consumption.
The Willis Tower in Chicago illustrates these considerations perfectly. Originally finished with black anodized aluminum when it opened in 1973, the building eventually showed its age as the anodizing oxidized and developed white spots. The solution? Complete replacement with Sherwin-Williams painted aluminum—a finish that can be maintained and touched up rather than requiring wholesale replacement when issues arise.
Understanding these distinctions positions you to make informed decisions for your specific applications. But once you've chosen paint as your finish, how do you navigate the vast world of color options and specialty finishes available?
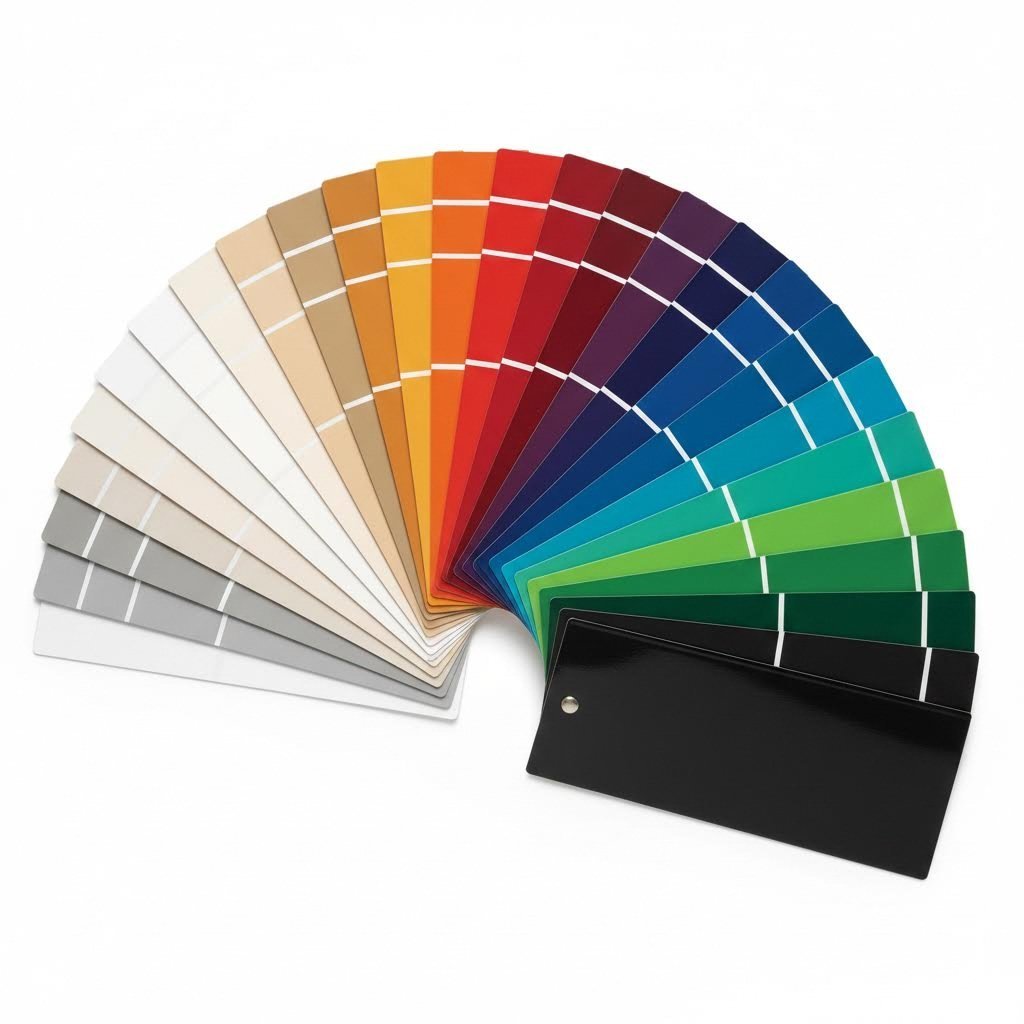
You've selected painted aluminum extrusions for your project—now comes the exciting part. What color? What sheen level? Should you consider specialty effects like wood grain or metallic finishes? The options available today extend far beyond basic colors, allowing architects and designers to achieve virtually any aesthetic vision while maintaining the durability standards covered in previous sections.
Whether you're specifying aluminum c channel components for a commercial facade or selecting c channel aluminum trim for interior applications, understanding the full spectrum of color and finish possibilities helps you make choices that enhance both form and function.
Imagine needing to match your painted extrusions precisely to your client's brand identity or coordinate with existing building elements. This is where standardized color systems become invaluable.
The RAL Classic color system offers over 200 carefully curated colors—from timeless neutrals like crisp whites and deep blacks to vibrant hues such as vivid yellows, striking reds, and rich violets. Because RAL colors are universally standardized, they ensure consistency across projects and manufacturing runs regardless of location or application.
What makes RAL particularly efficient? You can eliminate the need for physical sample chips in early selection stages. This streamlines approval processes, significantly reduces lead times, and eliminates much of the back-and-forth often associated with custom color matching. For projects requiring dependable color accuracy and faster turnaround times, RAL matching represents a smart, efficient choice.
Pantone color matching opens additional possibilities, particularly for brand-specific requirements. When a corporate client needs their exact brand blue across every visible aluminum component, Pantone codes provide the precision necessary for perfect replication.
Custom color matching takes flexibility further still. According to industry leaders, custom colors are excellent for projects demanding a personalized touch and distinct visual impact—whether institutional, commercial, healthcare-related, or residential. These finishes offer design flexibility that allows architects and designers to bring unique visions to life with precision.
Here's what to expect with custom color development:
Beyond color selection, finish type dramatically influences how your painted extrusions look and perform. Each finish level serves specific aesthetic and functional purposes.
When standard solid colors don't satisfy project requirements, specialty finishes open creative possibilities that were impossible just decades ago.
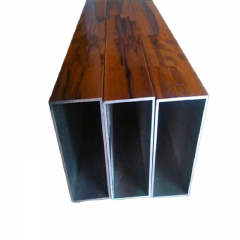
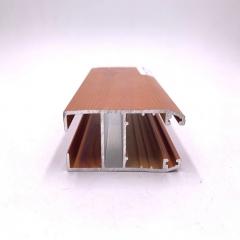
Wood grain finishes allow you to enjoy the warmth of natural wood aesthetics on aluminum substrates. Linetec offers more than 50 wood grain options achieved through powder coatings using a sublimation process. These textured specialty finishes meet AAMA 2604 standards and have proven resistant to corrosion, fire, high UV exposure, weathering, chemicals, and abrasion.
Why choose wood grain over actual wood? Unlike real wood, finished aluminum does not swell, rot, or warp. It resists termites and insects while eliminating seasonal staining, painting, and most other maintenance. These characteristics make wood grain finishes ideal for applications where traditional wood would prove cost-prohibitive or difficult to maintain.
Metallic and pearlescent finishes create sophisticated visual effects using aluminum paste and specialty pigments. According to coating specialists, these effects work particularly well for automotive, electronics, and consumer goods applications where a bright, modern appearance adds perceived value.
Anti-graffiti coatings address practical concerns in public spaces. These specialty surfaces allow easy removal of spray paint and markers without damaging the underlying finish—essential for transit facilities, urban buildings, and other vandalism-prone locations.
Sounds complex? Color consistency across large orders and multiple batches requires careful attention during specification and quality control.
When documenting color requirements in project specifications, include:
For projects spanning months or requiring future additions, request retained samples from your supplier. These reference chips ensure future orders match original installations—critical when replacing damaged components or expanding existing systems years later.
Understanding durability factors and maintenance requirements helps you select finishes that maintain their intended appearance throughout your project's lifespan—the focus of our next section.
You've invested in quality painted aluminum extrusions with carefully selected colors and appropriate AAMA specifications. Now comes an equally important consideration: how do you protect that investment over time? Even the highest-performance coatings require proper care to deliver their full lifespan potential. Understanding durability factors and establishing maintenance routines ensures your aluminum bar stock and finished components continue performing beautifully for decades.
Sunlight represents one of the greatest challenges facing any exterior coating. Ultraviolet radiation breaks down molecular bonds in paint films, causing gradual fading, chalking, and loss of gloss. But here's the good news: modern coating technologies have dramatically improved UV resistance compared to finishes available just twenty years ago.
How do different coating types compare under UV exposure? According to industry specifications, coating performance varies significantly:
Environmental factors compound UV effects significantly. Coastal locations with salt spray accelerate coating degradation. Industrial areas with airborne pollutants create chemical stress on paint films. Desert climates combine intense UV with temperature extremes that stress coatings through expansion and contraction cycles.
For aluminum bars used in exposed architectural applications, selecting the appropriate AAMA specification becomes critical. AAMA 2605 coatings demonstrate less than 5 Delta E color change after 10 years of South Florida exposure—a remarkably stable performance that justifies the premium cost for high-visibility installations.
Beyond UV exposure, painted aluminum extrusions face mechanical and chemical stresses that affect long-term performance. Understanding these factors helps you set realistic expectations and implement appropriate protective measures.
Corrosion protection depends on multiple factors working together. The aluminum substrate provides inherent corrosion resistance through its natural oxide layer. Proper pretreatment creates additional barrier protection. Finally, the paint film itself shields the metal from environmental attack. When any layer fails, the entire system becomes vulnerable.
Scratch resistance varies by coating type and thickness. Technical specifications indicate that quality coatings should achieve pencil hardness ratings of 3H or higher. This hardness level resists casual contact damage while remaining flexible enough to avoid cracking during thermal cycling.
What lifespan can you realistically expect? Under various conditions:
Here's something many overlook: high-quality architectural finishes are extremely durable, but even the best coatings still need regular attention. Establishing a maintenance routine prevents minor issues from becoming major problems.
For aluminum metal flat bar components and other painted extrusions, follow this recommended maintenance schedule:
What cleaning materials work best? Stick with pH-neutral cleaners diluted according to manufacturer instructions. Soft brushes, microfiber cloths, or low-pressure water effectively remove most contaminants without damaging finish surfaces.
Even with proper specification and maintenance, coating problems occasionally develop. Recognizing issues early and understanding their causes helps you address them effectively.
Adhesion failure typically indicates inadequate surface preparation before coating application. When paint peels or lifts from the aluminum substrate, the bond between metal and coating has broken down. Small areas may be repairable through touch-up procedures, but widespread adhesion failure often requires complete recoating.
Color inconsistency between building components usually stems from batch variations during manufacturing or differential weathering due to varying sun exposure. Preventing this issue requires specifying tight Delta E tolerances during ordering and ensuring consistent exposure conditions across similar components.
Coating damage from impact, abrasion, or chemical exposure requires prompt attention. According to finishing specialists, even with careful treatment during installation and daily use, occasional damage will occur. Minor scratches and chips can often be touched up using manufacturer-supplied repair materials. More extensive damage may require professional refinishing services.
Understanding warranty coverage protects your investment and sets appropriate expectations. But what should you look for when evaluating coating guarantees?
Key warranty elements to examine include:
Request warranty documentation before finalizing orders. Reputable suppliers provide clear written guarantees specifying exactly what's covered, for how long, and under what conditions. This documentation becomes valuable if issues arise years after installation.
With durability factors and maintenance requirements understood, you're ready to navigate the specification and ordering process—ensuring your painted extrusion project proceeds smoothly from initial concept through final installation.
You've explored coating methods, AAMA specifications, color options, and maintenance requirements. Now comes the practical challenge: how do you transform this knowledge into a successful order? Whether you're specifying aluminum channel track for a curtain wall system or selecting aluminium track channel for industrial equipment, the ordering process involves multiple decisions that directly impact project outcomes.
Think of specification as a roadmap. Without clear directions, even experienced suppliers struggle to deliver exactly what you need. Let's walk through the complete buyer journey—from initial research through final delivery—so you can navigate the process with confidence.
Every successful painted aluminum extrusion order begins with thorough specification. Incomplete or ambiguous requirements lead to delays, cost overruns, and disappointing results. What elements must your specification address?
Start with profile selection. Are you using standard aluminum extrusion shapes, or does your application require custom die development? Standard profiles—alu channel sections, angles, tubes, and bars—offer faster lead times and lower costs. Custom profiles provide design freedom but require tooling investment and additional production time.
According to industry guidance, picking the right alloy affects how strong and tough your parts will be. The 6000 series alloys dominate building applications, with 6061 offering high strength for structural components and 6063 providing smooth surfaces ideal for visible architectural elements. Both resist corrosion, weld easily, and machine cleanly.
Your alloy choice also influences finishing outcomes. Different alloys respond differently to pretreatment processes, potentially affecting coating adhesion and final appearance. Discuss alloy selection with your supplier early to ensure compatibility with your specified finish.
Sounds straightforward? Specifying color requires more precision than simply naming a shade. Effective color communication includes:
For aluminum c channel track applications in high-visibility areas, investing time in detailed color specification prevents costly rework. Request production samples before full manufacturing begins, particularly for large orders or projects where color consistency is critical.
Understanding the production timeline helps you plan realistic project schedules. What should you expect from order placement through delivery?
Industry data indicates typical lead times for custom extrusions range from 6 to 12 weeks after tooling approval. However, this timeline varies significantly based on several factors:
Tooling status dramatically influences delivery schedules. If new dies are required, the process includes design, die cutting, sample extrusion, validation, and potential refinement. Each step takes time, and unexpected issues during testing can add weeks to originally quoted timelines.
Minimum order quantities (MOQs) also affect project economics. Alum channel and alum c channel components in standard sizes typically have lower MOQs than custom profiles. Discuss volume requirements early—some suppliers offer flexibility for prototype quantities, while production orders may require larger commitments to justify setup costs.
How do you ensure delivered products meet your specifications? Establishing quality expectations upfront prevents disputes later.
Key quality control elements to address include:
Reputable suppliers maintain quality management systems certified to standards like ISO 9001. These certifications indicate systematic approaches to quality control rather than ad-hoc inspection processes.
Before submitting your order, verify that your specification addresses each critical element:
Your specification work means nothing if painted finishes are damaged before installation completes. Protecting coatings during handling, storage, and installation preserves the quality you've specified.
According to finishing experts, scratches and surface damage often occur during handling, cutting, or installation when protective measures are not taken. Sharp tools and improper storage exacerbate problems that could have been prevented.
Implement these protective practices:
Improper handling, excessive force during installation, or inadequate support can lead to buckling or warping that compromises both appearance and function. Following recommended guidelines ensures your aluminum track channel components and other painted extrusions arrive at final installation looking exactly as specified.
With specifications complete and handling procedures established, one question remains: who should manufacture your painted aluminum extrusions? Selecting the right partner significantly influences project success—the focus of our final section.
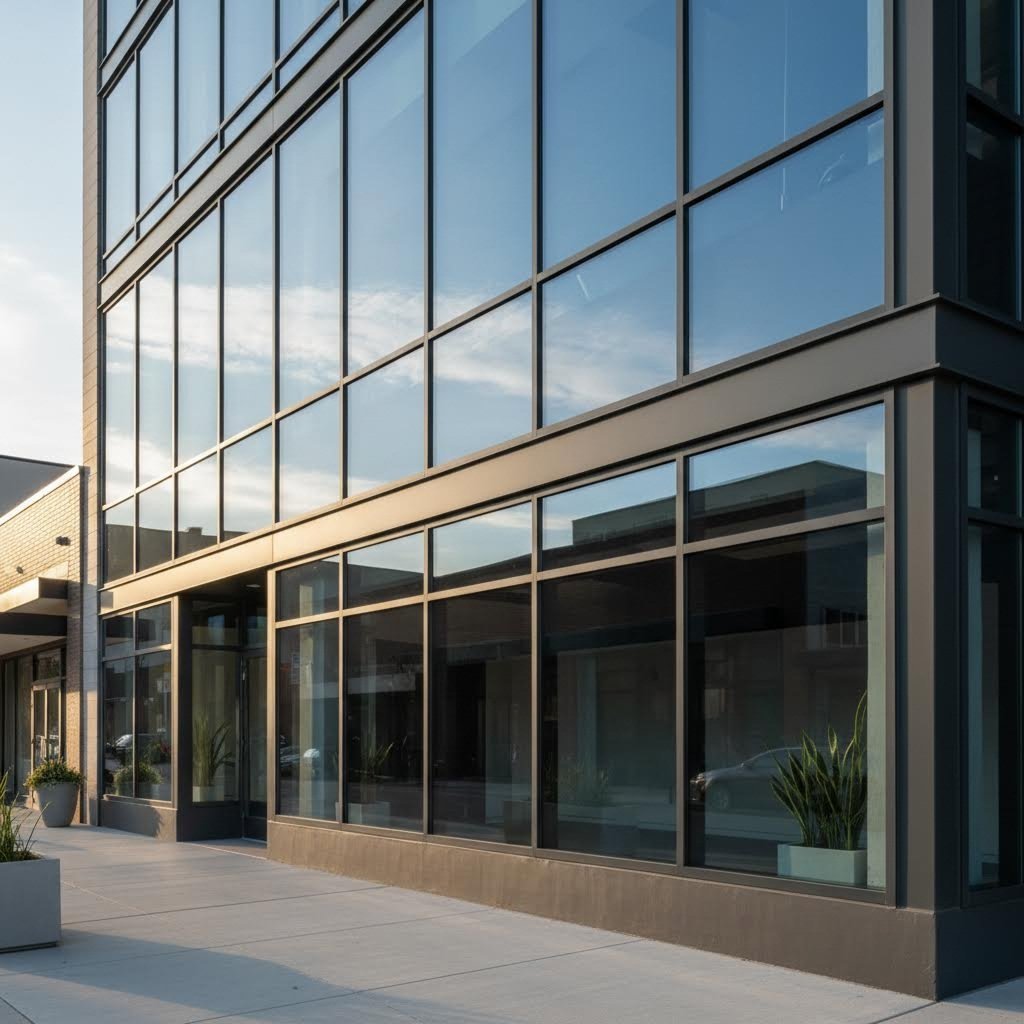
Where exactly do painted aluminum extrusions make the biggest impact? From towering commercial facades to precision industrial equipment, these versatile components serve applications across virtually every sector. Understanding where painted extrusions excel—and where alternative solutions might work better—helps you make confident decisions for your specific project requirements.
Let's explore the major application categories and build a practical framework for matching your needs to the right extrusion and finish combinations.
Walk through any modern city center, and you'll encounter painted aluminum extrusions everywhere you look. The building and construction sector represents the largest consumer of these finished profiles, and for good reason—they deliver the perfect balance of aesthetics, durability, and design flexibility.
Curtain wall systems showcase painted extrusions at their most visible. These non-structural facades rely on extruded aluminum tubing and framing members to support glass panels while creating seamless exterior appearances. With AAMA 2605 PVDF coatings, these systems maintain their color integrity for decades despite constant UV exposure and weathering.
Window and door frames represent another dominant application. Rectangular aluminum tubing and specialized frame profiles receive painted finishes that match architectural color schemes while providing excellent thermal performance. Unlike wood frames that require periodic refinishing, painted aluminum maintains its appearance with minimal maintenance.
Storefront systems depend on aluminum tubing rectangular profiles to create inviting retail environments. The unlimited color options available through powder coating and liquid finishes allow designers to reinforce brand identities while meeting demanding performance specifications.
Additional architectural applications include:
Beyond architecture, painted aluminum extrusions serve critical functions in manufacturing, automation, and commercial equipment. These applications often prioritize function alongside form—but appearance still matters.
Machine frames and safety enclosures rely heavily on aluminum extrusions according to industry applications research. Square aluminum tubing forms the structural backbone of automation systems, while painted finishes protect against factory environments and enhance equipment aesthetics.
Conveyor systems and material handling equipment utilize extruded aluminum tube components for lightweight yet durable construction. Painted finishes resist corrosion from humidity and provide visual differentiation between system components.
Cleanroom and controlled environment construction demands profiles that meet strict cleanliness requirements. Painted aluminum with smooth, sealed surfaces prevents particle accumulation and enables easy sanitization—critical for pharmaceutical, semiconductor, and food processing facilities.
Consider these additional industrial applications:
Painted aluminum extrusions extend into consumer-facing products where brand aesthetics and product differentiation drive material selection. Furniture manufacturers specify painted profiles for modern designs. Sporting goods companies use lightweight painted aluminum for equipment frames. Electronics enclosures feature anodized or painted finishes that complement product branding.
Transportation applications—from recreational vehicle trim to marine components—leverage painted aluminum's corrosion resistance and color stability. Solar panel mounting systems increasingly specify painted profiles that blend with roofing materials while resisting decades of outdoor exposure.
How do you determine whether painted aluminum extrusions fit your project? This decision framework helps you evaluate key factors and match them to appropriate solutions.
| Project Requirement | Recommended Profile Type | Suggested Finish | Key Considerations |
|---|---|---|---|
| High-visibility exterior facade | Custom architectural profiles | AAMA 2605 PVDF (70% fluoropolymer) | Maximum color retention; 10+ year warranty; custom color matching available |
| Commercial storefront framing | Standard window/door profiles | AAMA 2604 high-performance polyester | Balance of performance and cost; 5-year color retention; wide color selection |
| Interior architectural trim | Decorative channels and angles | AAMA 2603 powder coating | Cost-effective for protected environments; unlimited color options |
| Industrial equipment frames | T-slot and structural profiles | Standard powder coating | Durability over aesthetics; scratch resistance important; modular assembly |
| Cleanroom construction | Smooth-surface profiles | Smooth powder coat or liquid finish | Sealed surfaces prevent contamination; chemical resistance required |
| Marine or coastal installation | Heavy-wall profiles | AAMA 2605 with marine-grade pretreatment | Salt spray resistance critical; premium pretreatment essential |
| Brand-specific color matching | Application-dependent | Custom color development | Pantone or custom matching; sample approval before production; allow extra lead time |
| Wood appearance preferred | Flat or shaped profiles | Sublimation wood grain finish | AAMA 2604 performance; 50+ patterns available; no maintenance like real wood |
Complex projects often require capabilities beyond basic extrusion and painting. When your application demands custom profiles, specialized finishes, and precision fabrication, partnering with manufacturers offering comprehensive services streamlines the entire process.
What capabilities should you look for in a full-service provider?
For example, Shengxin Aluminium's deep processing services demonstrate how integrated capabilities support diverse project requirements. Their surface treatment options include powder coating in custom colors, anodizing with specialty finishes like champagne and rose gold, PVDF coatings, and micro-arc oxidation for enhanced durability. This range allows architects and engineers to source complete solutions—from raw extrusion through finished, fabricated components—through a single partner.
Such comprehensive capabilities prove particularly valuable when projects require:
Whether your project involves architectural facades demanding premium PVDF finishes or industrial equipment requiring durable powder-coated frames, matching your specific requirements to appropriate extrusion and finish combinations ensures optimal outcomes. The decision framework above provides starting guidance, but detailed discussions with qualified suppliers refine these recommendations for your unique application.
With applications understood and requirements matched to solutions, one critical decision remains: selecting the right manufacturing partner to bring your painted extrusion project to life.
You've defined your project requirements, specified the right AAMA performance tier, and selected colors that perfectly complement your design vision. Now comes perhaps the most consequential decision of all: who will manufacture your painted aluminum extrusions? The supplier you choose directly influences product quality, delivery reliability, and ultimately, project success.
Think about it this way—even the most detailed specification means little if your manufacturing partner lacks the equipment, expertise, or quality systems to execute it properly. Whether you're sourcing aluminum t bar profiles for architectural trim, aluminum z channel components for industrial framing, or complex custom extrusions for specialized applications, the right partner transforms specifications into reality.
What separates a capable supplier from an exceptional one? Start by examining these critical capability areas:
Production Equipment and Capacity
According to industry selection guidance, your supplier's production capacity must align with your project scope and technical demands. Key questions to explore include:
Suppliers with diverse press capabilities—ranging from smaller tonnage for precision profiles to large-capacity presses for substantial structural extrusions—offer flexibility that single-press operations cannot match.
Surface Treatment Options
A manufacturer's finishing capabilities determine what colors and performance levels they can deliver. Evaluate whether potential suppliers offer:
In-house finishing generally improves quality control and reduces lead times compared to outsourced operations. When evaluating finishing capabilities, confirm whether these services are performed on-site or through subcontractors—this distinction affects both turnaround time and quality consistency.
Quality Certifications and Systems
Reliable suppliers demonstrate their commitment to quality through certifications and documented processes. Industry experts emphasize that ISO 9001 certification means the manufacturer follows strict quality rules, providing assurance that systematic quality controls govern every production step.
Beyond certification, examine the supplier's quality control practices:
Technical Support and Engineering Expertise
The best suppliers function as technical partners rather than mere vendors. Look for manufacturers offering:
This expertise proves invaluable when working with aluminum z bar profiles, z channel aluminum components, or other specialized shapes where design optimization significantly impacts both manufacturing efficiency and product performance.
Before committing to a manufacturing partner, gather answers to these critical questions:
Projects flow smoothly when a single partner manages the entire production chain—from initial die development through mass production and finishing. This integrated approach delivers several advantages:
Accountability: One supplier owns the entire outcome rather than pointing fingers between extrusion and finishing partners.
Efficiency: Eliminating handoffs between facilities reduces lead times and minimizes handling damage risks.
Consistency: Unified quality systems ensure profiles and finishes meet specifications throughout production.
Communication: A single point of contact simplifies project management and problem resolution.
Consider how this works in practice. Shengxin Aluminium exemplifies comprehensive capability with over 30 years of industry experience and 35 extrusion presses ranging from 600T to 5500T capacity. Their integrated services span die development, extrusion, and complete surface treatment options including powder coating, PVDF, anodizing in custom colors like champagne and rose gold, and micro-arc oxidation for enhanced durability.
Whether you need aluminum t bars for architectural framing, precision alum t bar profiles for equipment housings, or clip on metal components requiring exact color matching, such comprehensive providers support projects from concept through delivery. Their technical teams provide guidance on optimizing designs for both extrusion efficiency and finishing performance—the kind of collaborative expertise that prevents problems before they occur.
Ready to move forward? Here's how to launch your project effectively:
The time invested in supplier evaluation pays dividends throughout your project. A partner with the right equipment, quality systems, and technical expertise transforms your painted aluminum extrusion specifications into components that perform beautifully for decades.
Don't underestimate the value of leveraging your supplier's experience. The best manufacturers have solved challenges similar to yours countless times. Their insights on alloy selection, finish specification, and design optimization can save you time, reduce costs, and improve outcomes. Approach the relationship as a collaboration rather than a transaction, and you'll unlock the full potential of painted aluminum extrusions for your project.
Yes, extruded aluminum can be painted using powder coating or liquid coating methods. However, proper surface preparation is essential for lasting adhesion. This includes thorough cleaning, chemical etching, and applying conversion coatings before painting. Without these preparation steps, paint will eventually peel from aluminum's naturally smooth surface. Professional finishing services like those offered by Shengxin Aluminium ensure proper pretreatment and AAMA-certified coating application for durable, long-lasting results.
Painted aluminum extrusion lifespan varies by coating type and environment. Regular polyester coatings carry 3-5 year warranties, while high-performance PVDF coatings offer 15-20 year warranties with proper maintenance. AAMA 2605-certified finishes demonstrate less than 5 Delta E color change after 10 years of outdoor exposure. Factors affecting longevity include UV exposure, coastal salt spray, industrial pollutants, and maintenance frequency. Regular cleaning and prompt touch-up of damaged areas extend finish life significantly.
For industrial applications, powder coatings and liquid coatings specifically formulated for aluminum provide the best adhesion. Powder coatings are electrostatically applied and thermally cured at 350-400°F, creating extremely durable finishes. Liquid options include polyesters, siliconized polyesters, and fluoropolymers like PVDF. The key to successful adhesion is proper pretreatment—cleaning, etching, and conversion coating create the micro-texture and bonding layer that keeps paint firmly attached to the aluminum surface.
AAMA specifications define coating performance tiers. AAMA 2603 suits interior and mild exterior use with optional one-year weathering tests. AAMA 2604 requires mandatory five-year color retention testing, making it ideal for commercial storefronts with 10-year warranties. AAMA 2605 is the premium specification demanding ten years of color and chalk resistance, typically using PVDF coatings with 20-year warranties. Choose based on exposure conditions—interior projects need 2603, commercial exteriors benefit from 2604, and high-visibility architectural facades require 2605.
Both finishes excel in different scenarios. Painted aluminum offers unlimited color options, better batch-to-batch consistency (2 Delta E tolerance), and field-repairable surfaces—ideal for custom color projects and facades. Anodized aluminum provides sapphire-like hardness and superior abrasion resistance, making it better for high-traffic areas like handrails. However, anodizing limits color choices and cannot be touched up in the field. For maximum design flexibility with long-term color retention, AAMA 2605 painted finishes often prove superior for architectural exteriors.


 Интернет Сервис
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 русский
 English
 français
 Deutsch
 español
 português
 العربية
 ไทย
 Việt
 Українська